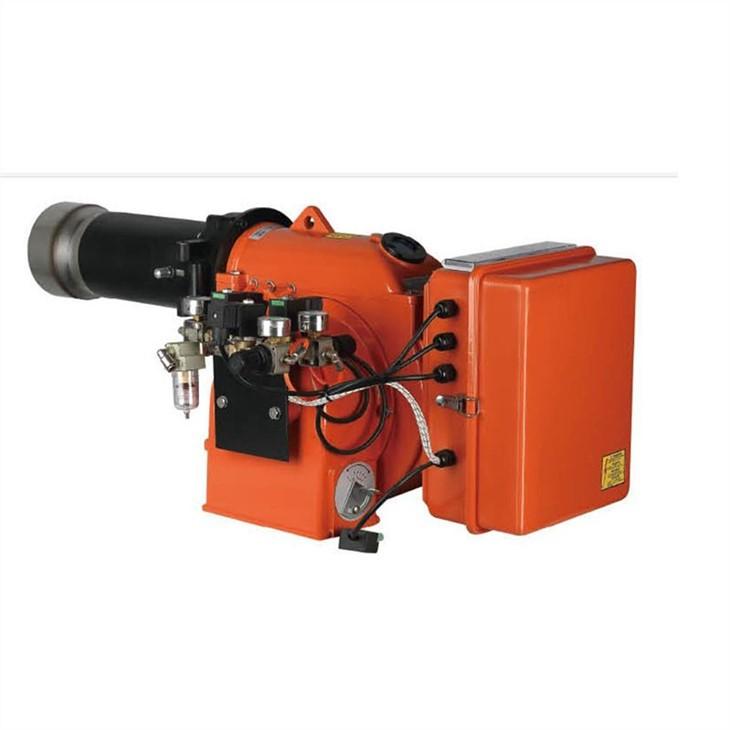
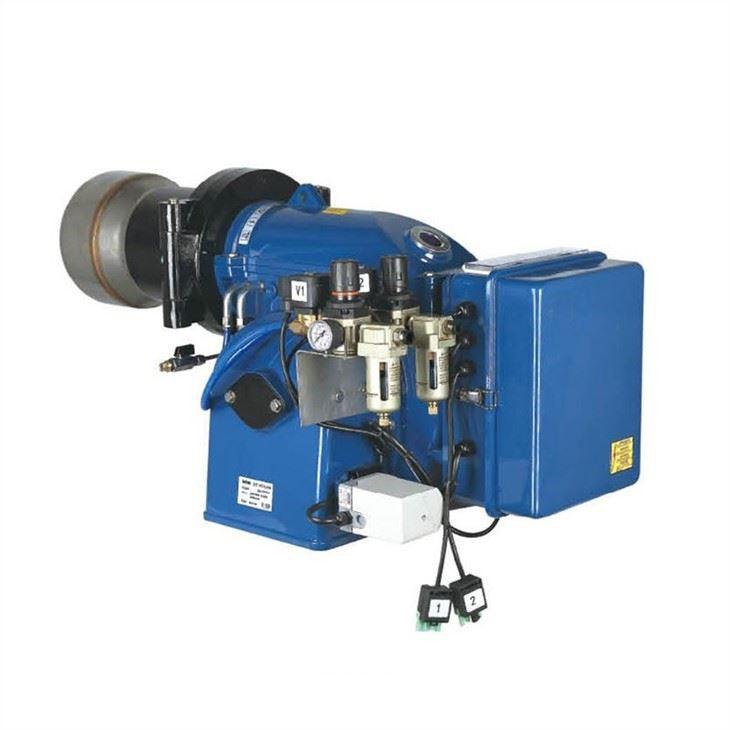
BNTET Pyrolysis / Refinery Byproduct Oil Burner Series
The BNTET Pyrolysis and Refinery Byproduct Oil Burner Series is engineered for seamless integration with industrial boilers, rotary kilns, asphalt mixing plants, and heavy-duty thermal systems. It ensures the safe, highly efficient atomization and combustion of highly viscous pyrolysis oils, refinery residues, and variable waste oils to achieve optimal, cost-effective thermal output. Equipped with advanced oil pre-heating systems and specialized atomization technology to handle high impurities and fluctuating viscosities, along with smart automation, this series provides a robust, reliable thermal solution tailored for demanding heavy industrial heating and waste-to-energy applications.Features
High-Volume Heavy Oil Processing
Offering impressive thermal output and high heavy-fuel throughput while maintaining a compact, modular skid-mounted design for easy transportation and rapid industrial installation.
Anti-Clogging High-Flow Atomization
Features a specialized wide-channel nozzle system and heavy-duty pre-heating pipelines that seamlessly accommodate high-viscosity pyrolysis oils, refinery residues, and fluid impurities without clogging.Other Features
- Advanced Pre-Heating & Atomization Technology – Ensures complete and stable combustion of highly viscous oils while actively reducing soot to meet environmental regulations.
- Intelligent Control Interface – Allows precise, independent adjustment of oil pre-heating temperatures and air-fuel ratios to maximize thermal efficiency.
- Anti-Clogging Wide-Channel Nozzles – Robust, heavy-duty fuel delivery design that seamlessly accommodates high-viscosity oils and fluid impurities without blockages.
- Automated Flame Safety Interlocks – Comprehensively protects operators and equipment by instantly sealing oil valves and deactivating the system in the event of flame failure or pressure anomalies.
- Simplified Maintenance & Filter Access – Features easily accessible heavy-duty oil filters and quick-release nozzle assemblies, allowing safe and efficient cleaning of oil impurities during downtime.
- Steam/Air Assist Atomization Ready – Optional modular configurations utilizing compressed air or steam to forcefully break down heavy residues, further minimizing soot and emissions.
- Corrosion & Wear-Resistant Components – Manufactured from premium specialized alloys designed to withstand the abrasive and corrosive properties (such as sulfur) inherent in refinery byproducts, ensuring a remarkably long service life.
Applications
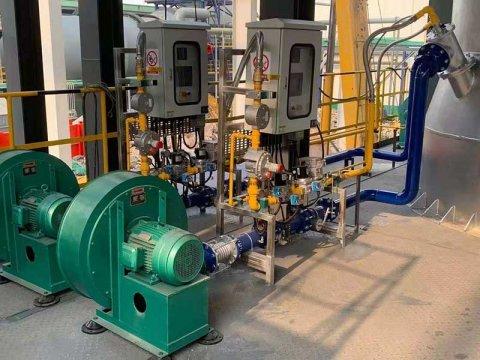
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.