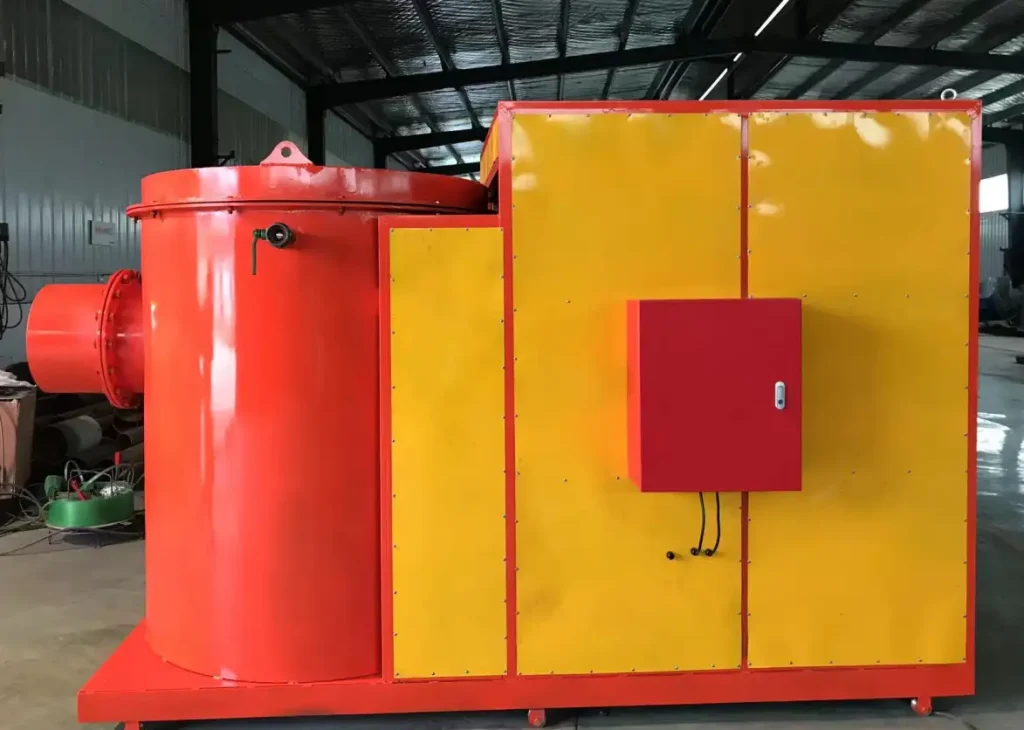
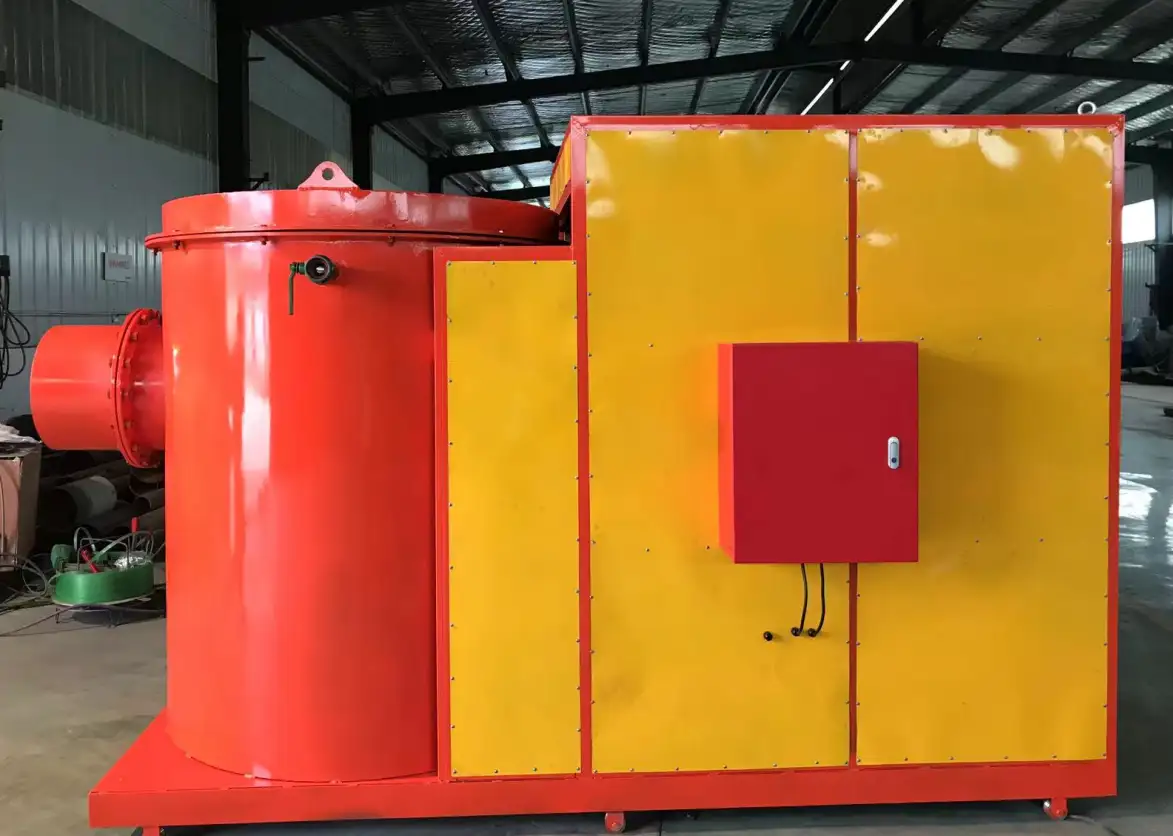
Biomass Gas Burners Series
The BNTET Biomass Gas Burner Series is engineered for industrial boilers and thermal systems transitioning to renewable energy. It delivers consistent thermal output by maximizing the efficiency of low-calorific biomass syngas. Equipped with specialized tar-resistant gas trains and smart automation to handle fluctuating gas compositions, it provides a highly reliable, carbon-neutral solution for demanding waste-to-energy applications.Features
Exceptional Biomass Syngas Utilization
Our industrial biomass gas burners are engineered to handle varying qualities of low-calorific syngas with ease, making them ideal for waste-to-energy facilities and industrial plants transitioning to renewable energy. With optimized thermal output capabilities and specialized gas trains designed to accommodate pressure fluctuations, moisture, and high tar content, our systems ensure highly efficient fuel processing without compromising on flame stability or carbon-neutral compliance.
Advanced Engineering for Variable Gas Conditions
Every BNTET biomass gas burner system is built with cutting-edge gas-air mixing technology tailored for low-calorific fuels and rigorous safety-focused functionality. From specialized impurity-tolerant combustion heads and robust tar-resistant gas valves to smart automation panels that seamlessly adjust to fluctuating gas compositions, our burners are precisely designed for maximum thermal efficiency, continuous operation, and long-term durability in demanding waste-to-energy environments.Other Features
- Low-Calorific Combustion Technology – Ensures complete and highly stable combustion of low-calorific biomass syngas, overcoming the challenges of fluctuating gas quality while meeting strict carbon-neutral environmental standards.
- Intelligent Control Interface – Features an advanced panel that seamlessly adjusts air-gas ratios in real-time to compensate for fluctuating biomass gas compositions, maximizing continuous thermal efficiency.
- Tar-Resistant Gas Delivery System – Robust, wide-channel gas train design specifically engineered to prevent blockages from tar, moisture, and particulate impurities commonly found in unrefined biomass syngas.
- Automated Flame-Out Protection & Safety Interlocks – Comprehensively protects operators and equipment by instantly sealing gas valves in response to flame failure caused by sudden gas pressure drops or exceptionally low heating values.
- Simplified Maintenance Access – Features an easily accessible combustion head and ignition layout, allowing safe and highly efficient cleaning of accumulated tar and ash during routine maintenance.
- Eco-Friendly Emission Optimization – Engineered to maximize the combustion of raw syngas while minimizing unburned hydrocarbons and CO emissions, ensuring a clean, carbon-neutral waste-to-energy operation.
- Corrosion-Resistant Combustion Head – Manufactured from premium specialized alloys designed to withstand the corrosive effects of moisture and trace acids in biomass gas, ensuring a remarkably long service life in harsh environments.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.