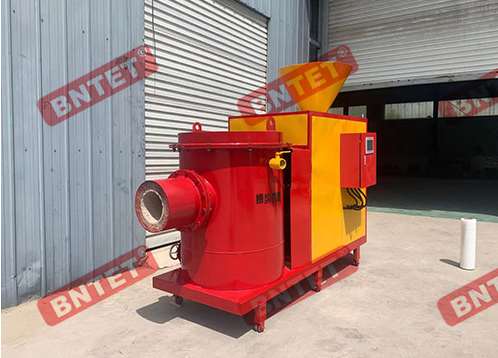
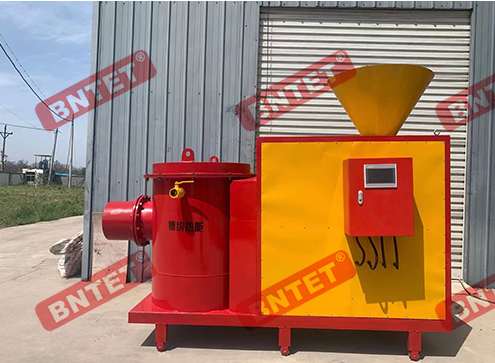
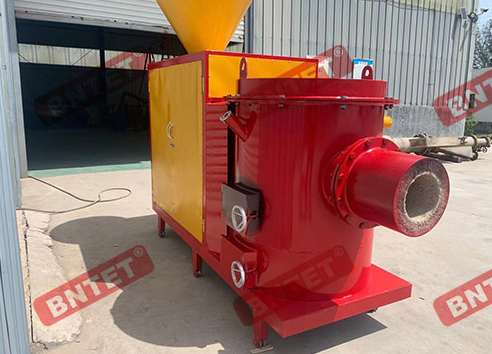
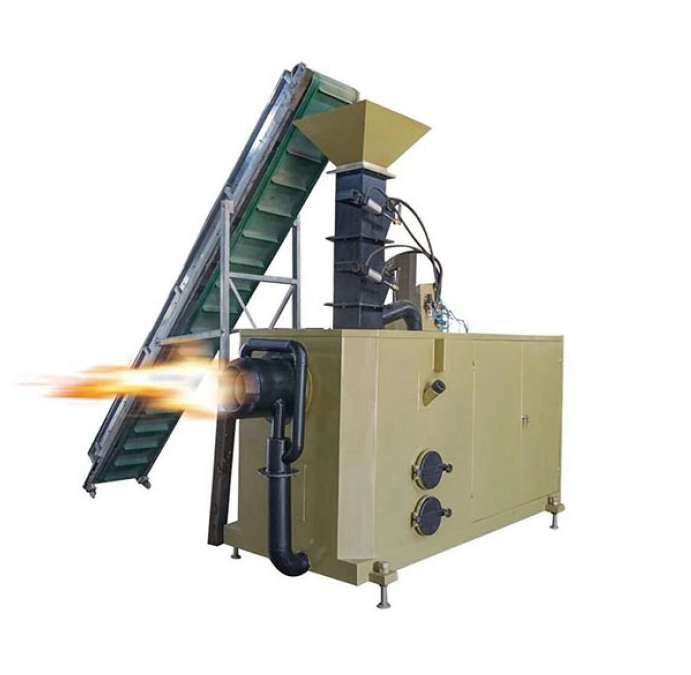
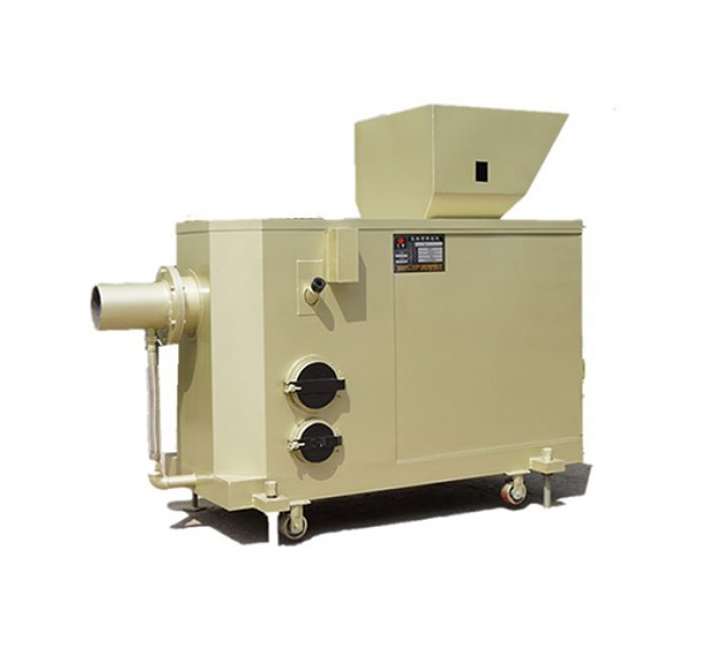
BNBP Series Biomass Burner
This versatile combustion accessory has earned its popularity through reliable multi-fuel functionality, effectively handling wood pellets, sawdust, and various agricultural residues. Its advanced semi-gasification technology ensures complete fuel burnout with minimal ash residue and ultra-low carbon emissions.Featuring a practical automated auger feeding interface, the BNBP series simplifies continuous fuel delivery operations, making it a highly adaptable choice for upgrading existing kilns and heating systems. Despite its space-efficient footprint, this core combustion component maintains impressive heat transfer rates and exceptional operational efficiency.
Features
Superior Thermal Performance
The BNBP Biomass Burner series delivers exceptional combustion throughput, providing a highly consistent, high-volume thermal output that eliminates energy bottlenecks in demanding industrial applications. Engineered with advanced anti-clogging auger and aeration dynamics, the system ensures reliable, non-stop operational capacity while minimizing maintenance downtime. Combined with continuous 24-hour operation capability and superior versatility in processing diverse biomass pellet types, it ensures seamless energy delivery, making it the ultimate high-capacity solid-fuel combustion accessory.
Advanced Environmental Compliance
The precision-engineered BNBP burner delivers an exceptional 95% combustion efficiency through optimized semi-gasification technology and a multi-stage airflow system that ensures comprehensive fuel burnout. By facilitating precise, intensive air-biomass mixing and supporting internal combustion staging, the system sustains a highly stable flame geometry. This effectively minimizes particulate matter and NOx generation at the combustion source, ensuring full compliance with stringent international environmental and emission standards.Why Choose BNFT Series Split-Type Burners?
- Advanced Semi-Gasification Technology: Ensures high-efficiency, complete biomass combustion while strictly meeting modern environmental emission regulations.
- Smart Integrated Control Panel: Allows precise, independent adjustment of fuel feed rates and air distribution for optimized thermal efficiency.
Other Features
- Automated Auger Feeding Interface –A streamlined, heavy-duty mechanical system that ensures simple, consistent, and continuous biomass pellet delivery.
- Automated System Interlock – Protects the industrial furnace and operators by instantly deactivating the burner if optical sensors detect combustion anomalies or system pressure irregularities.
- Maintenance-Friendly Ash Access – Features an accessible port design, allowing safe and quick removal of residual ash during scheduled maintenance intervals.
- Modular Emission Control Compatibility – Designed to integrate seamlessly with downstream secondary environmental equipment, such as bag filters or scrubbers, to further minimize emissions.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
Technical Specifications
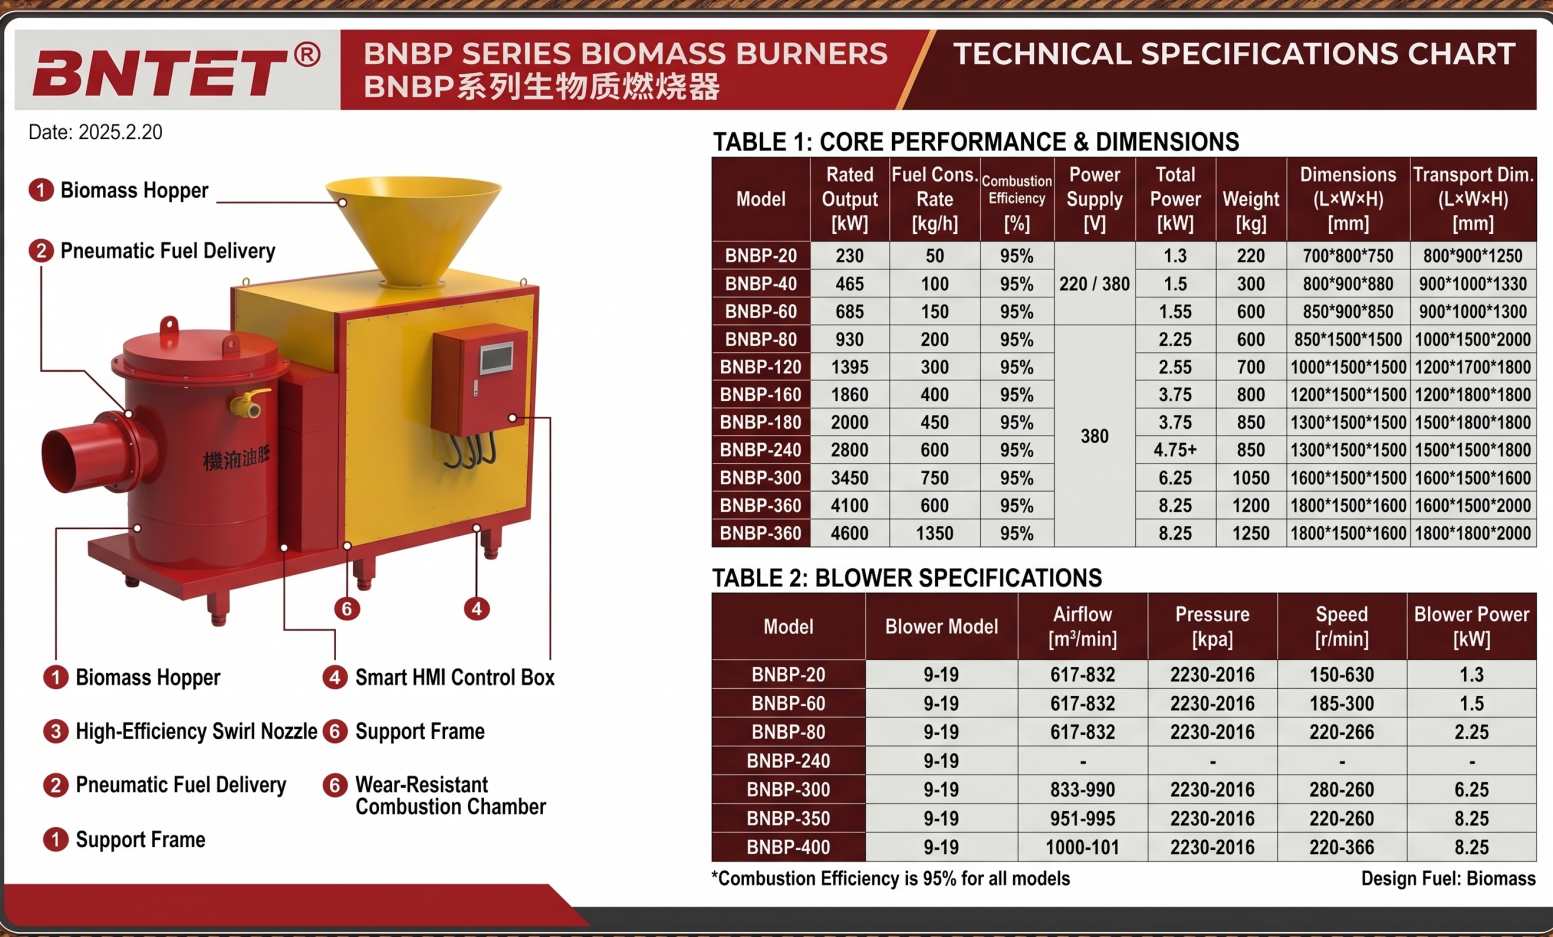
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.