BNFT Series Split-Type Burners
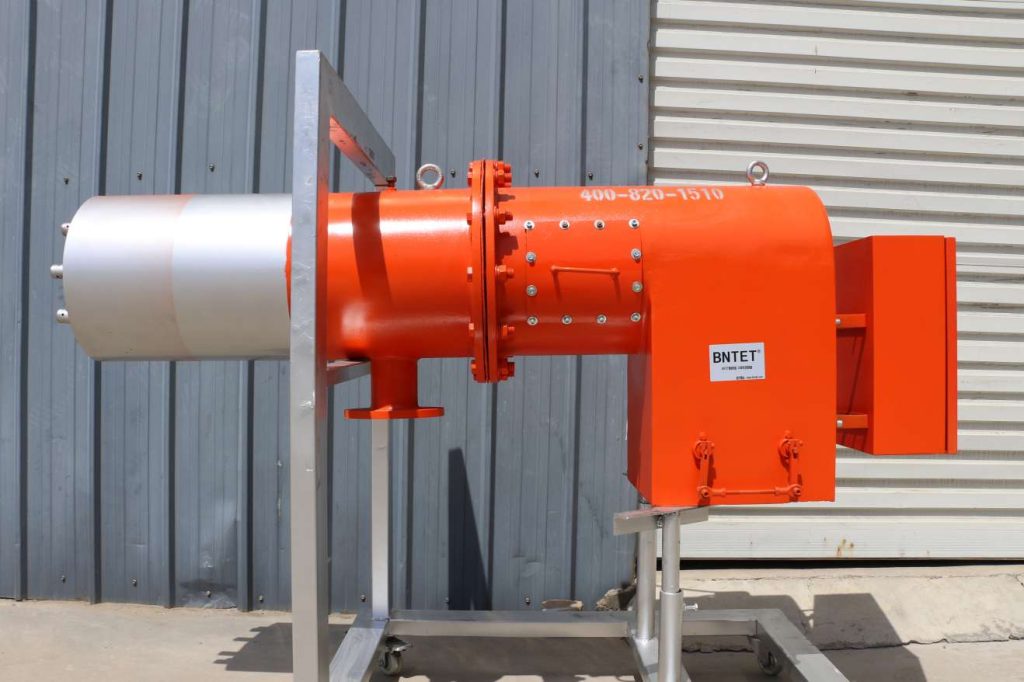
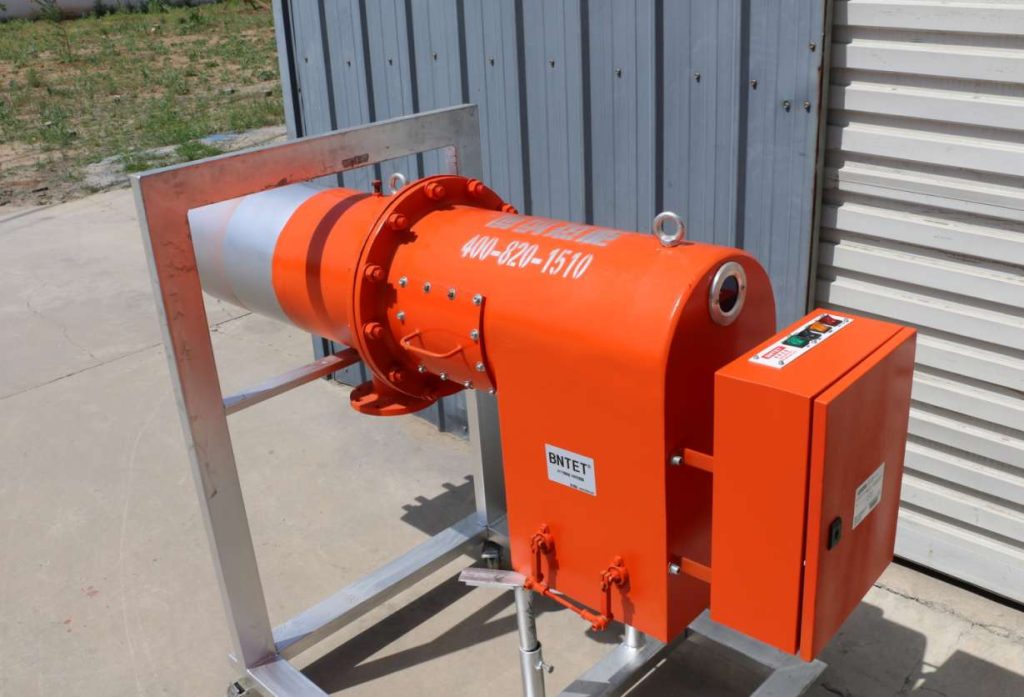
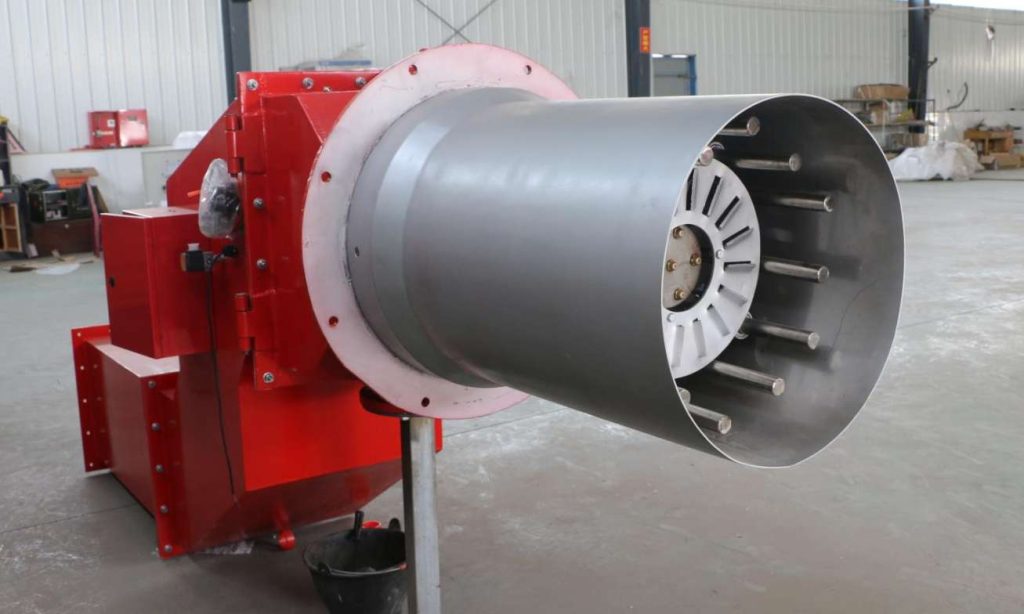
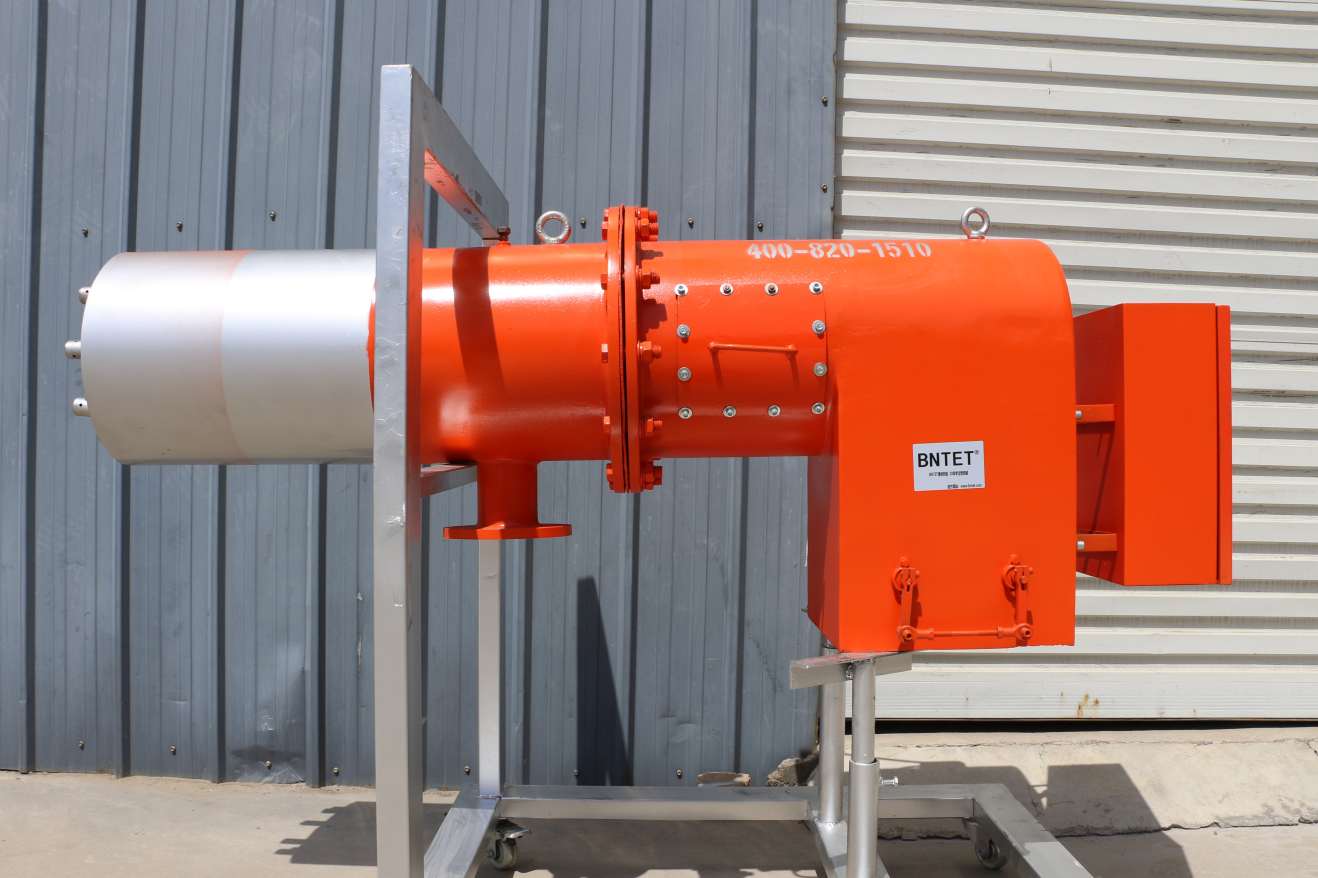
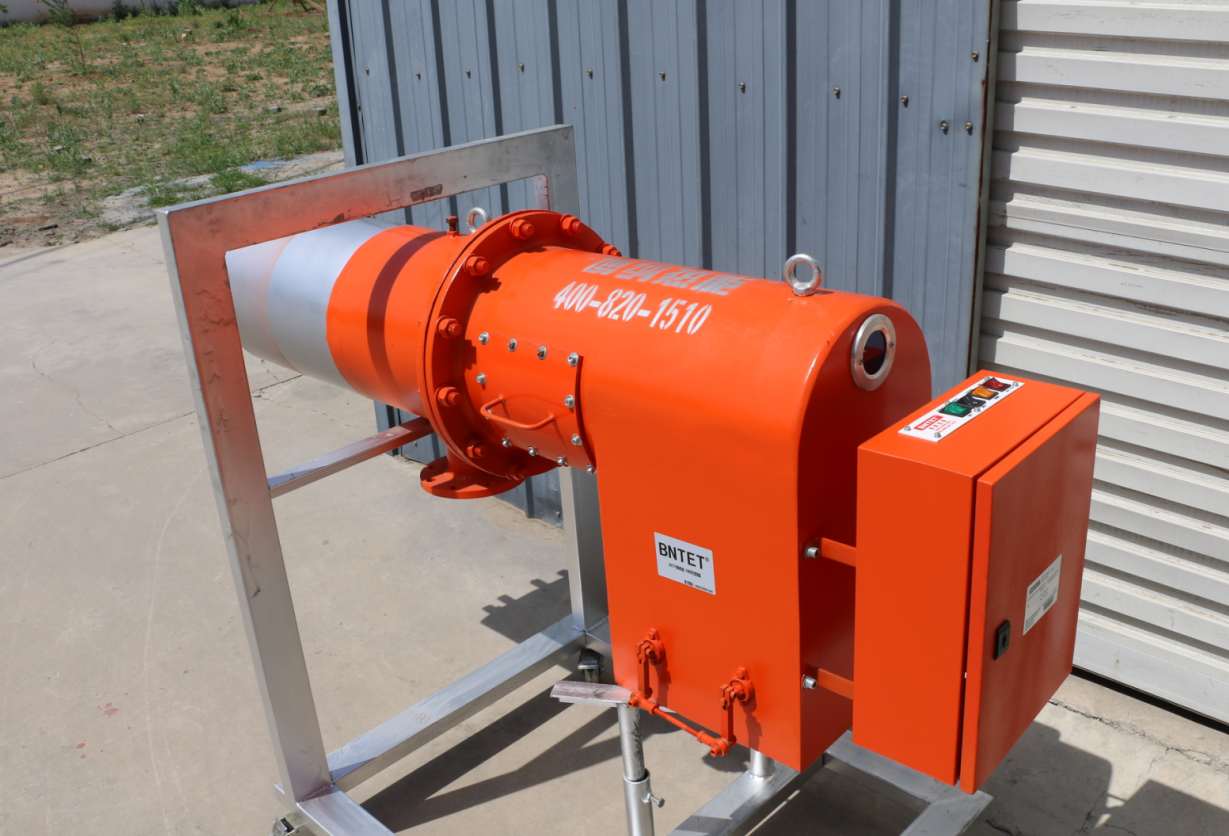
The BNFT series split type burner is at the forefront of combustion technology, offering an impressive wide power range and supreme combustion efficiency while still achieving some of the lowest NOx emissions in its class. The BNFT series can be customized with specialized fan configurations and advanced electronic-scale control systems to provide an effective and sustainable thermal energy solution for diverse heavy industries with massive heating demands. It also benefits from smart programmable controllers and remote monitoring technology, allowing operators to view combustion performance and live 24-hour flame diagnostics from anywhere in the world.Features
Superior Thermal Performance
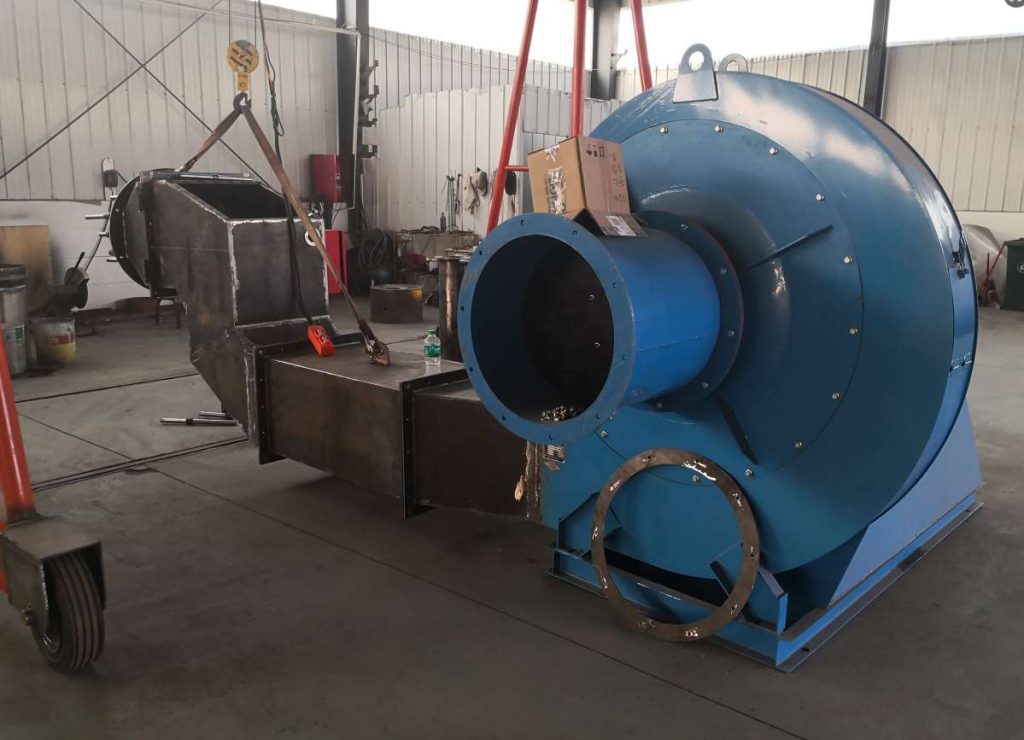
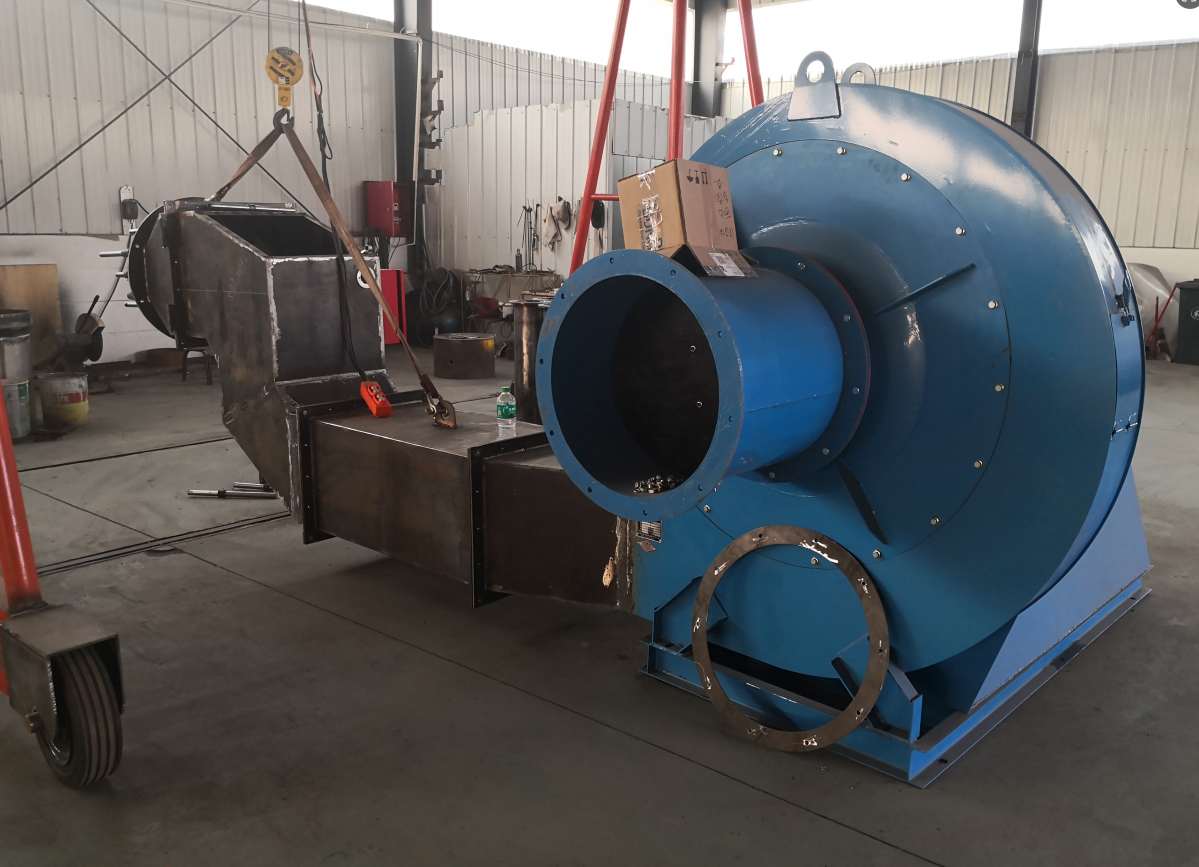
The BNFT series delivers an immense thermal output of up to 22,000 kW, effortlessly meeting the most demanding large-scale industrial heating requirements. Its innovative separated fan design and easily accessible internal components minimize maintenance downtime. Combined with continuous 24-hour operation capability and versatile dual-fuel (gas and heavy oil) compatibility, it ensures seamless energy delivery, making it the ultimate high-capacity combustion solution.
Advanced Environmental Compliance
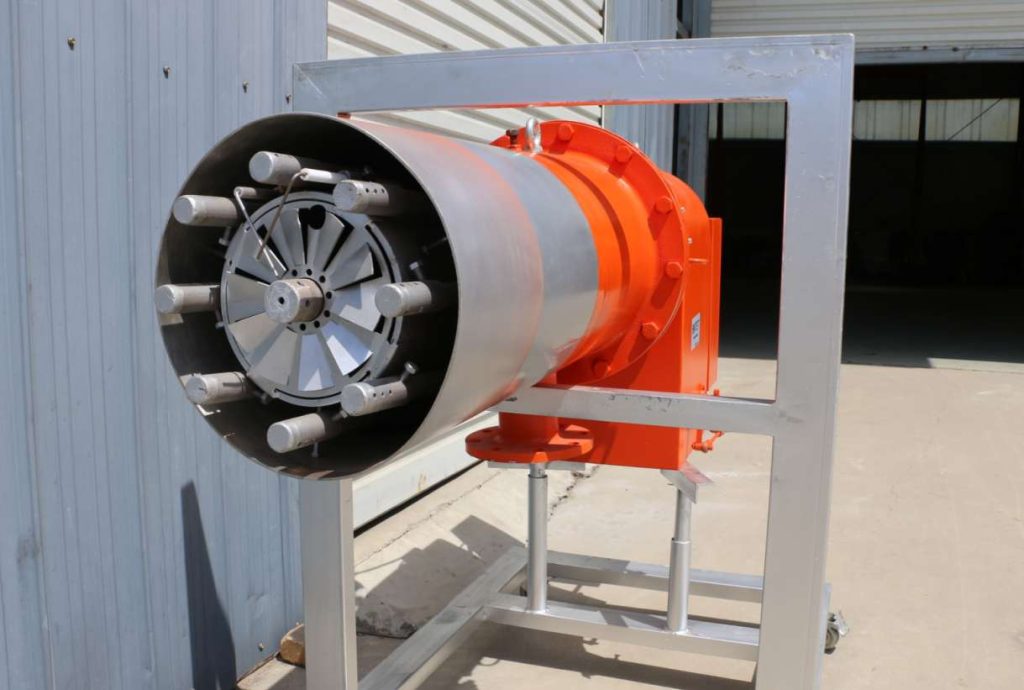
The BNFT burner series delivers exceptionally clean combustion through its advanced air-fuel intensive mixing technology and custom-angled gas sprayer heads, which significantly decrease NOx discharges. Operating with a supremely accurate electronic adjusting ratio and optimized combustion aerodynamics, it ensures complete fuel oxidation, effectively maximizing thermal efficiency while meeting stringent international environmental and emission standards.Why Choose BNFT Series Split-Type Burners?
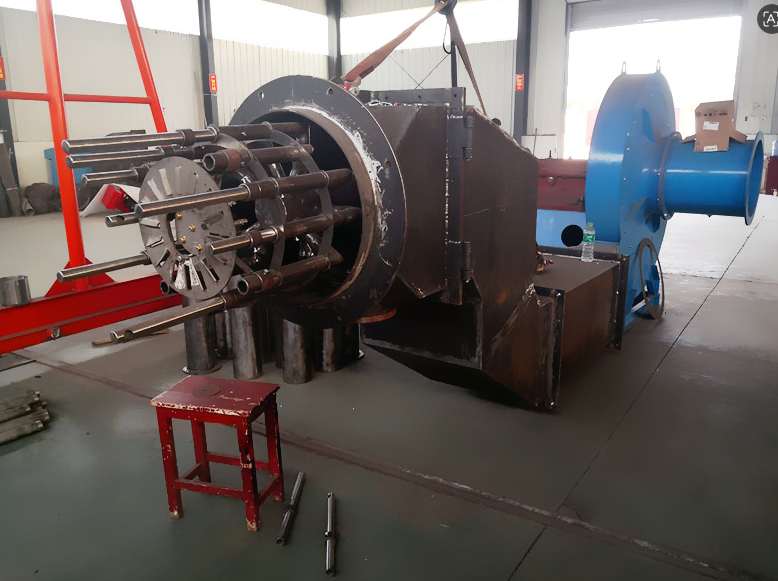
- Enhanced Operational Safety: The separated configuration intrinsically isolates the blower from the combustion head. Combined with automated safety protocols and full-seal top-cover access, it comprehensively protects operators during high-capacity startup and maintenance, ensuring a reliable and hazard-free environment.
- Optimized Thermal Dynamics: Engineered with advanced airflow dynamics and central air diffusers for intensive air-fuel mixing, maximizing energy recovery and maintaining consistent heat transfer for both heavy oil and gas in demanding industrial applications.
Other Features
- Advanced Integrated Safety Systems – Offers robust operator and equipment protection featuring 24-hour continuous flame signal self-detection by the program controller and automated fuel-shutoff protocols for safe heavy-duty operation.
- Intelligent Modulation Control – Features a sophisticated electronic-scale control interface with optional VFD (Variable Frequency Drive) integration, allowing for supremely accurate air-fuel ratio modulation and efficient dual-fuel combustion management.
- Automated High-Volume Fuel Control – Ensures effortless and precise regulation of large-scale heavy oil and gas flows using premium automated valve trains, specifically designed to withstand the rigors of heavy-duty, high-capacity industrial boilers.
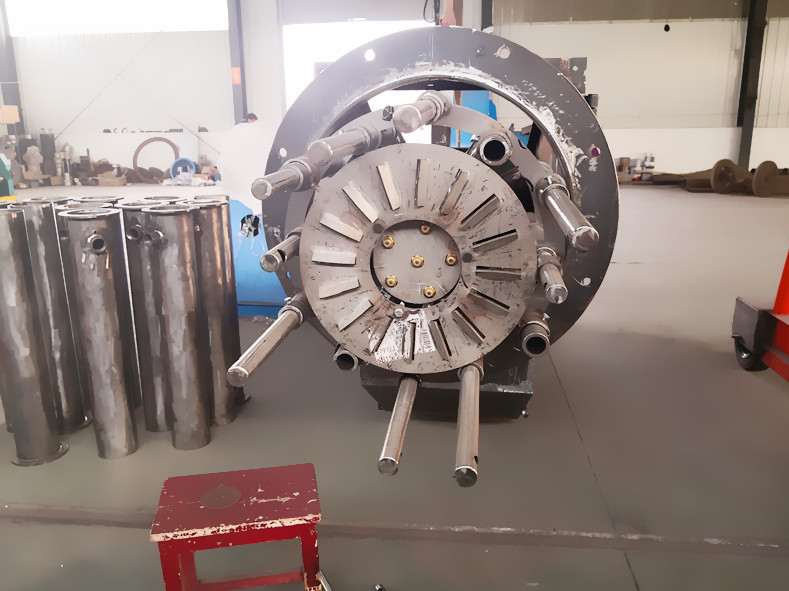
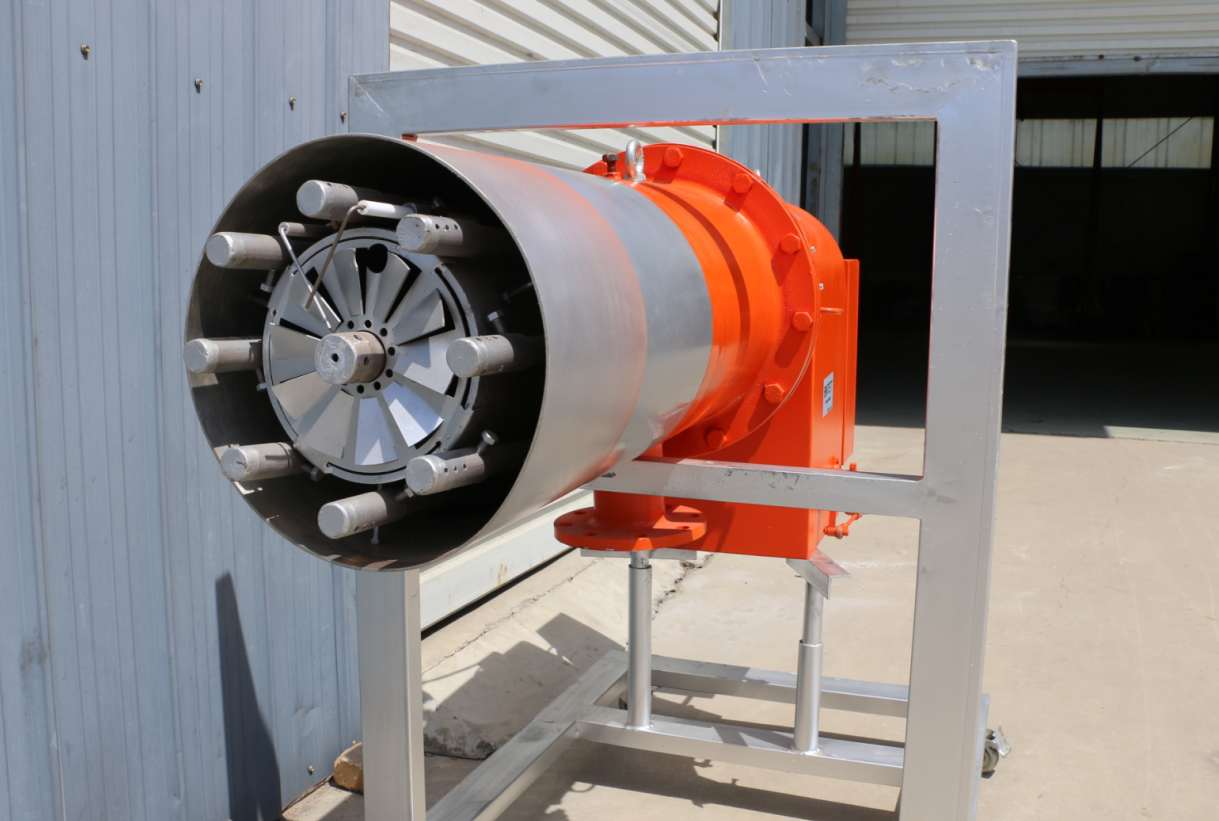
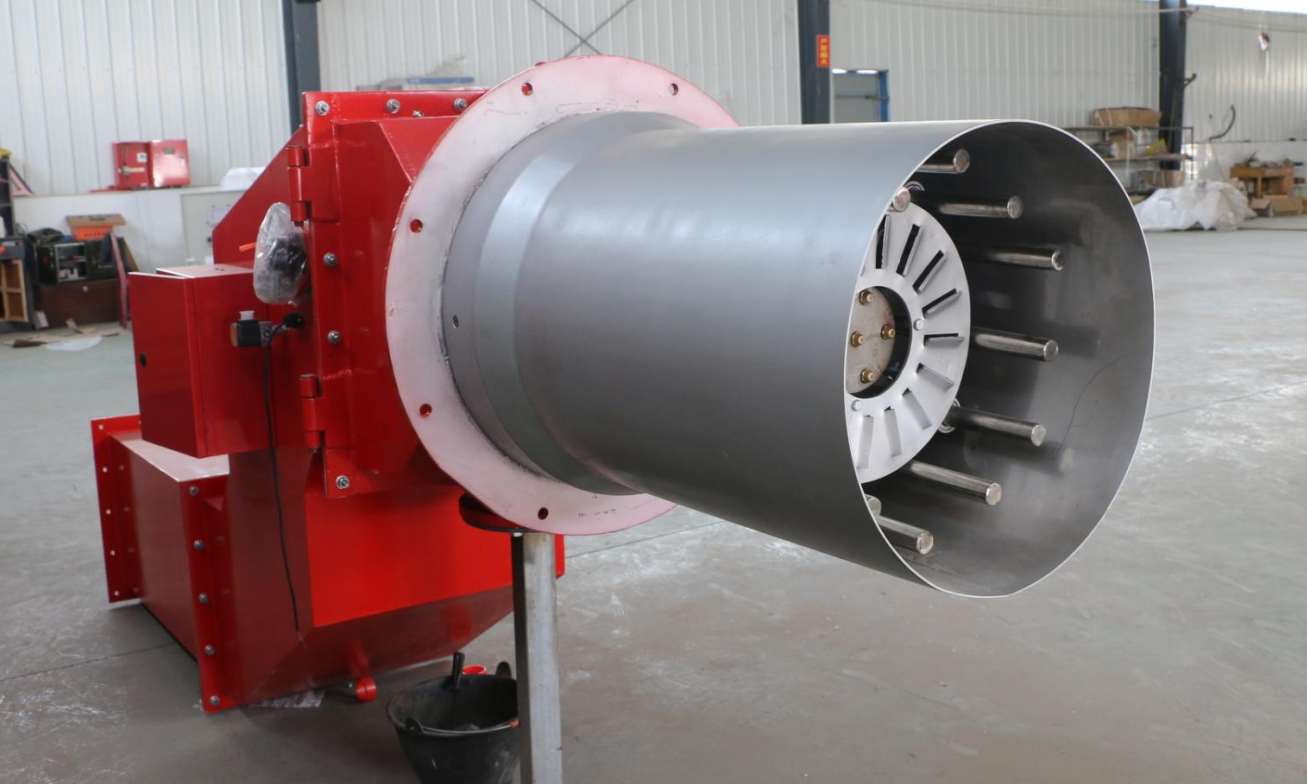
- Optimized Combustion Head Design – Features custom-angled gas sprayer heads and strategically distributed nozzles around the central air diffuser, delivering superior aerodynamics for intense mixing, enhanced flame stability, and reduced NOx emissions.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
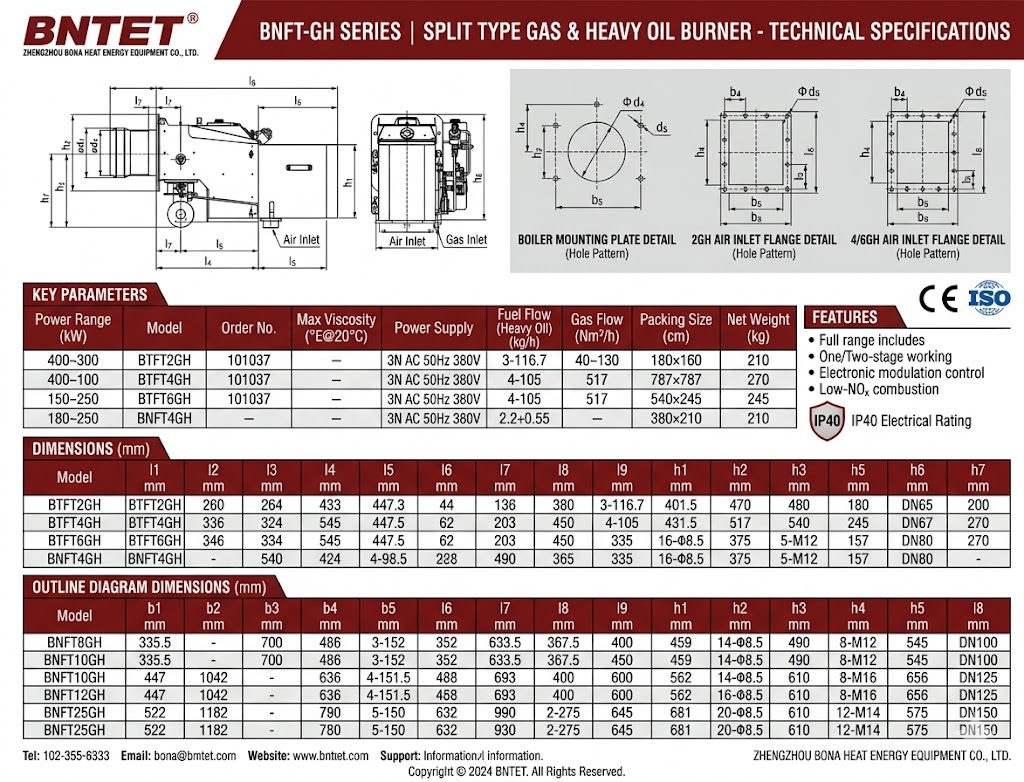
Technical Specifications
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.