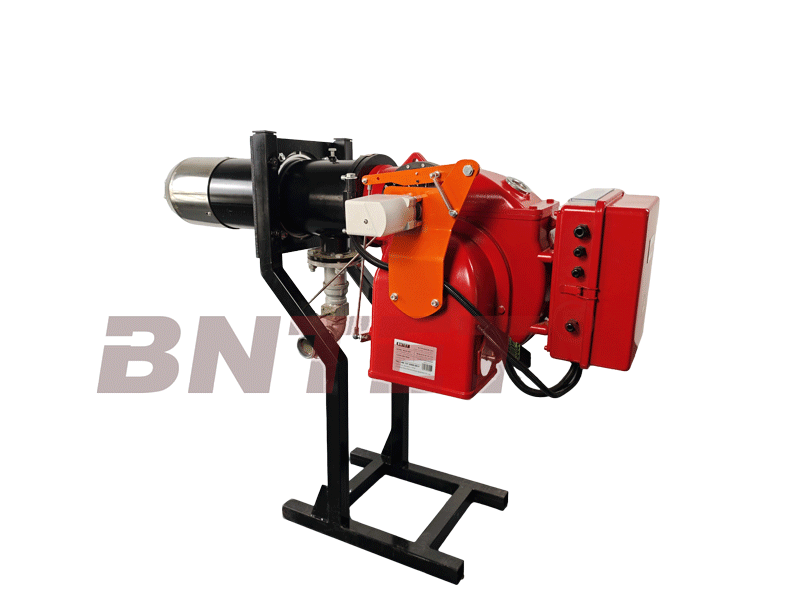
BNG-150P Industrial Gas Burner
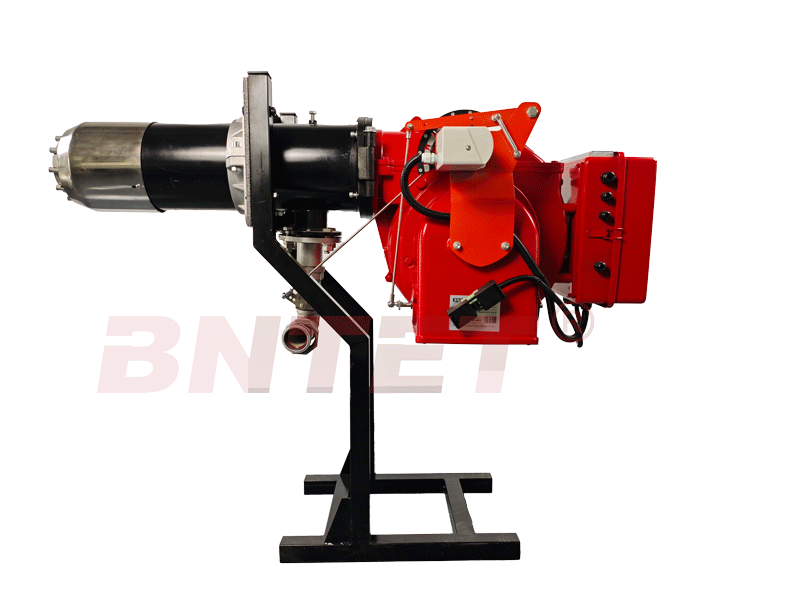
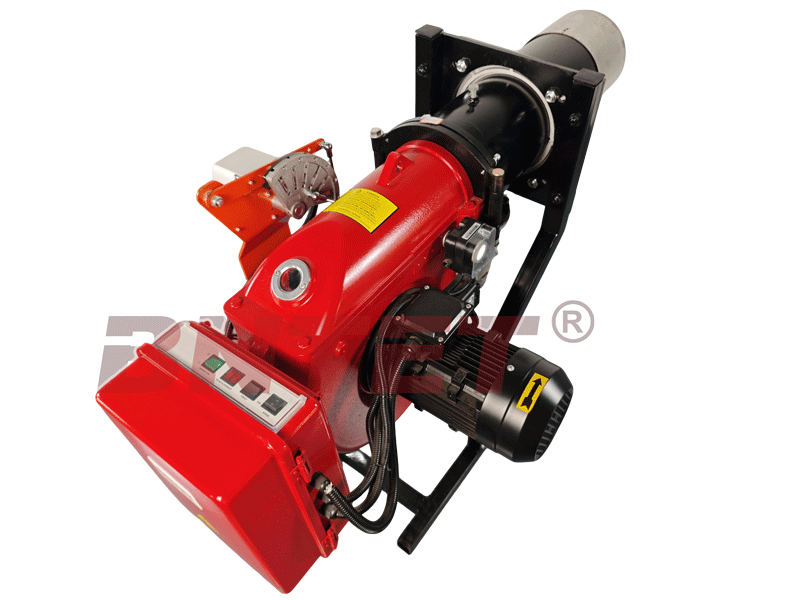
The BNTET BNG-15 Gas Burner stands out as a highly efficient, compact industrial gas burner designed for reliable combustion and stable heat output. Engineered for small to medium-scale heating applications, this versatile burner system is ideal for boilers, hot air generators, and other thermal processing equipment requiring precise and low-emission combustion performance. The BNG-15 delivers stable ignition, intelligent control, and dependable operation, making it the perfect solution for commercial heating systems, light manufacturing, and facilities with limited installation space.Features
High-Capacity Precision Thermal Control
Engineered to provide robust heat output for large-scale industrial boilers and furnaces. Its dual-stage operation capability ensures that the burner transitions smoothly between low and high fire, maintaining precise temperature stability even during peak production cycles.
Sophisticated Air-Gas Management for Optimized Efficiency
Features an advanced air-gas mixing system at the blast-pipe, ensuring complete combustion and maximum fuel utilization. Operators can fine-tune the combustion air and blast-pipe parameters to achieve peak thermal efficiency, significantly lowering operational fuel costs.Why Choose BNG-150P Industrial Gas Burner?
- Engineered for Low-Downtime Maintenance: The modular design allows the atomisation unit to be removed effortlessly for routine inspection and cleaning without the need to detach the main burner body from the boiler. This drastically reduces maintenance time, keeping your production line running longer.
- Robust Versatility & Adaptability: The integrated sliding coupling flange allows for precise adjustment to varying boiler head protrusions. This universal adaptability, combined with a secure insulating seal, ensures a perfect, leak-free mechanical installation across a wide spectrum of industrial boiler types.
Other Features
- Reliable Flame Safety Assurance – Equipped with a high-sensitivity ionisation electrode for continuous, instant flame monitoring and system protection.
- Durable Industrial-Grade Protection – Certified with an IP40 protection rating, ensuring the internal electrical plant remains shielded against solid ingress and harsh environmental conditions.
- Precise Air Flow Control – Equipped with adjustable air intake and electric servomotor control for accurate combustion air regulation.
- Precision Calibration – Includes a dedicated combustion air intake with a fine-adjustment device, allowing for exact control over every combustion parameter.
- Flexible One/Two-Stage Operation – Supports single-stage or two-stage working modes to meet different industrial heating requirements.
- Stable & Efficient Combustion – Optimised air-gas mixing and adjustable combustion settings ensure stable flame performance and high combustion efficiency.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
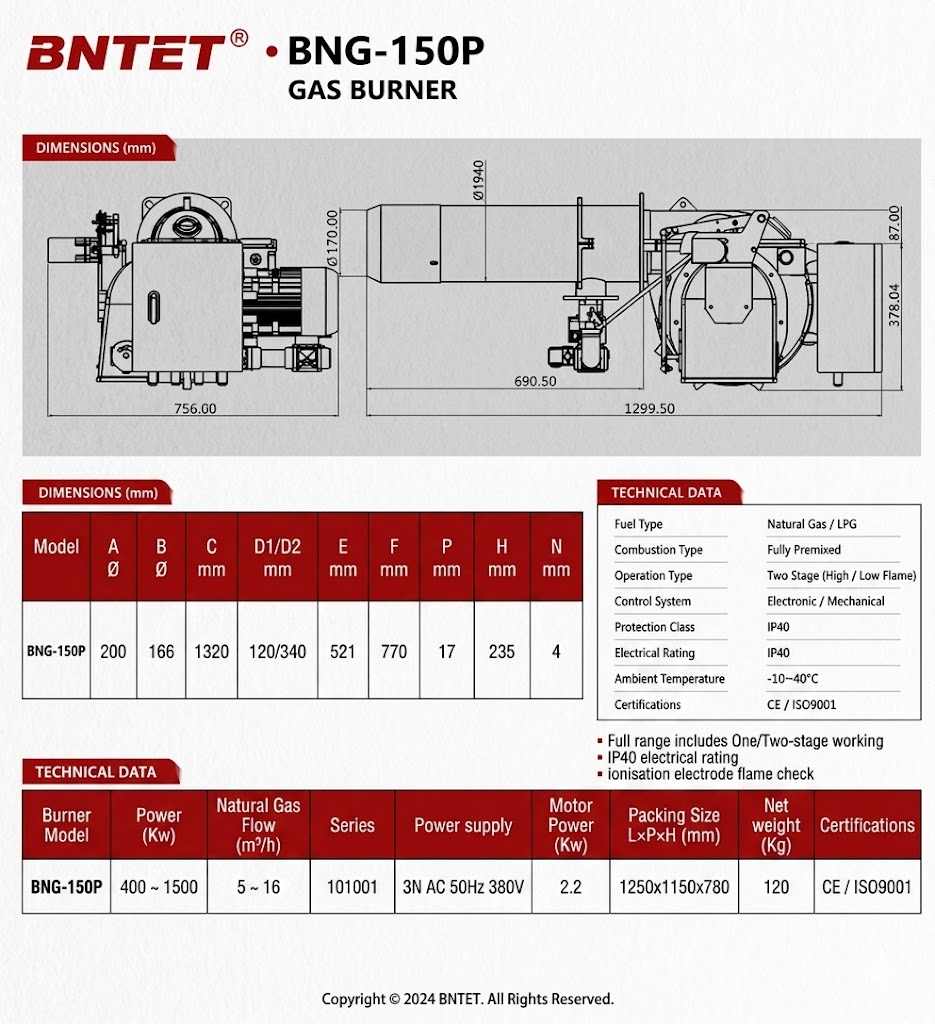
Technical Specifications
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.