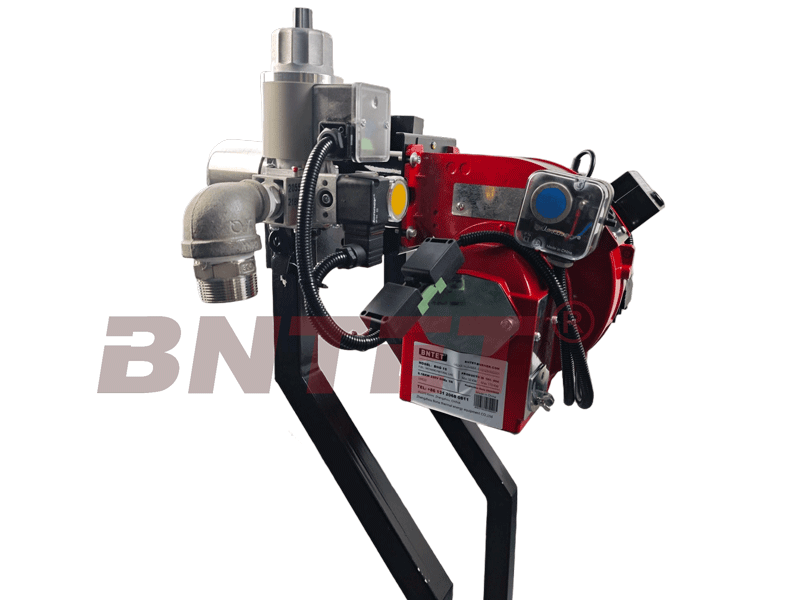
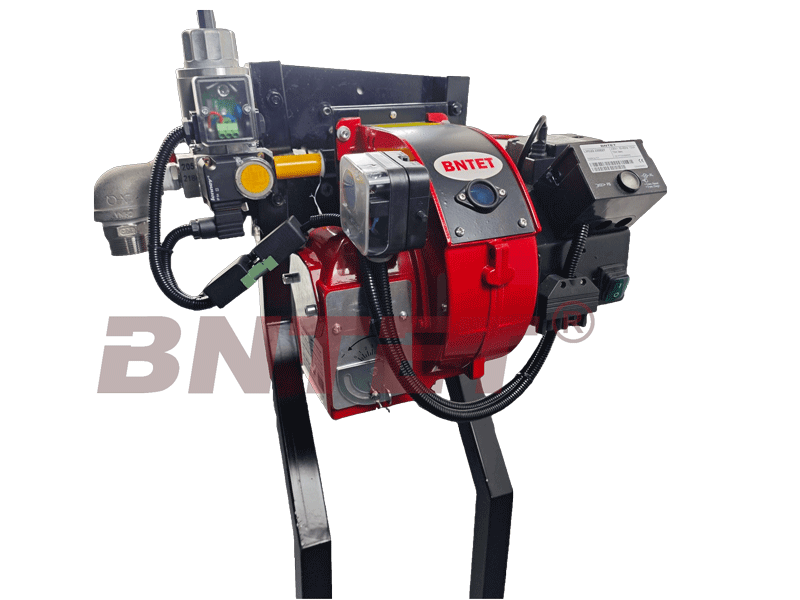
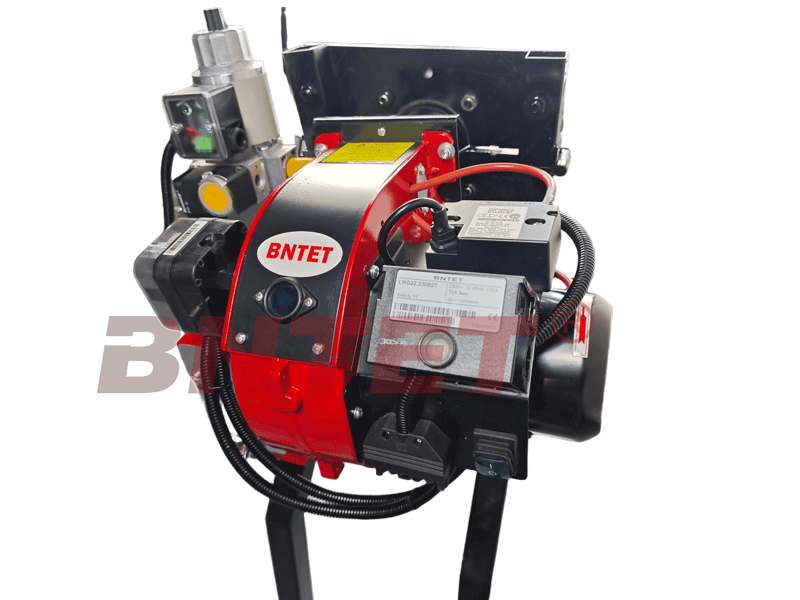
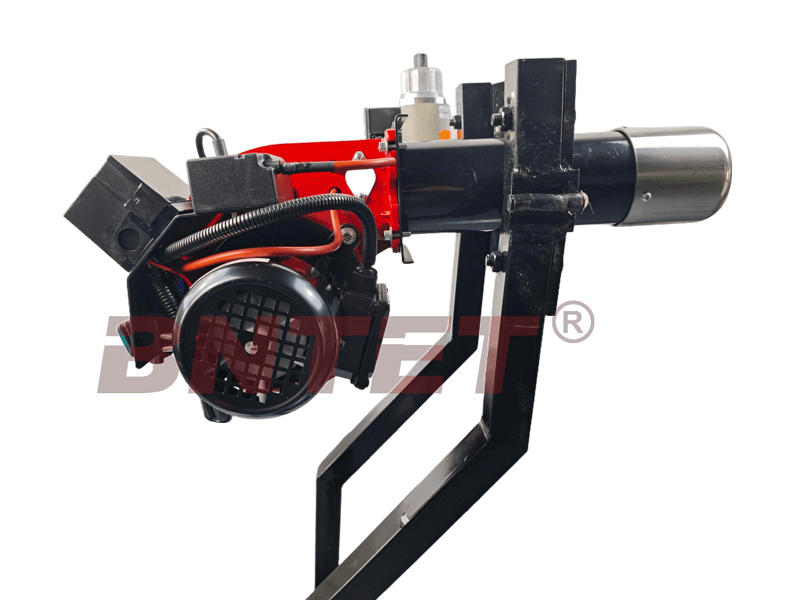
BNG-15 Gas Burner
The BNTET BNG-15 Gas Burner stands out as a highly efficient, compact industrial gas burner designed for reliable combustion and stable heat output. Engineered for small to medium-scale heating applications, this versatile burner system is ideal for boilers, hot air generators, and other thermal processing equipment requiring precise and low-emission combustion performance. The BNG-15 delivers stable ignition, intelligent control, and dependable operation, making it the perfect solution for commercial heating systems, light manufacturing, and facilities with limited installation space.Features
Optimized Combustion Efficiency
Features advanced air-gas mixing directly at the blast-pipe. Operators can easily regulate both combustion air and the blast-pipe to consistently achieve optimal combustion values and fuel savings.
Industrial-Grade Safety & Reliability
Powered by a robust monophase electric motor and protected by an IP40 electrical rating. Continuous safety is guaranteed through precise flame presence monitoring via an ionisation electrode.Why Choose BNG-15?
- Flexible Operational Control: Available in both one-stage and two-stage working configurations to seamlessly adapt to your specific load requirements and production demands.
- Compact Power: Engineered for high output with a minimal footprint, making integration and maintenance easier than ever.
- Highly Adaptable Installation: Equipped with a sliding boiler coupling flange, one standard flange, and an insulating seal, allowing it to easily adapt to the head protrusions of various types of boilers on the market.
Other Features
- Reliable Safety Protection – Integrated ionisation electrode flame detection and IP40 electrical protection improve operational safety and stability.
- Wide Boiler Compatibility – Sliding coupling flange design allows easy installation on various types of industrial boilers.
- Precise Air Flow Control – Equipped with adjustable air intake and electric servomotor control for accurate combustion air regulation.
- Easy Maintenance Design – The removable combustion unit allows convenient maintenance without removing the burner from the boiler.
- Flexible One/Two-Stage Operation – Supports single-stage or two-stage working modes to meet different industrial heating requirements.
- Stable & Efficient Combustion – Optimised air-gas mixing and adjustable combustion settings ensure stable flame performance and high combustion efficiency.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
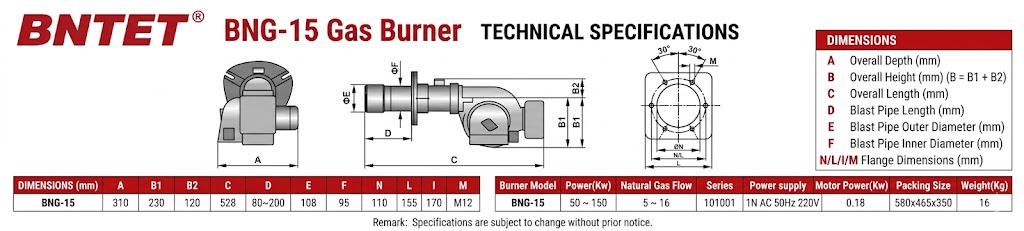
Technical Specifications
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.