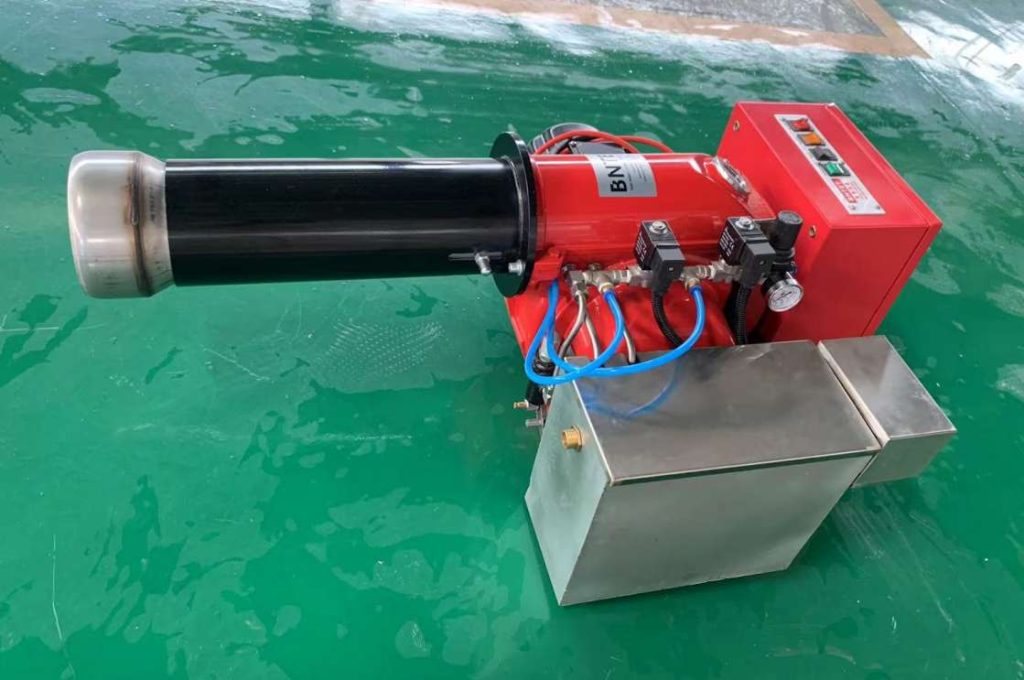
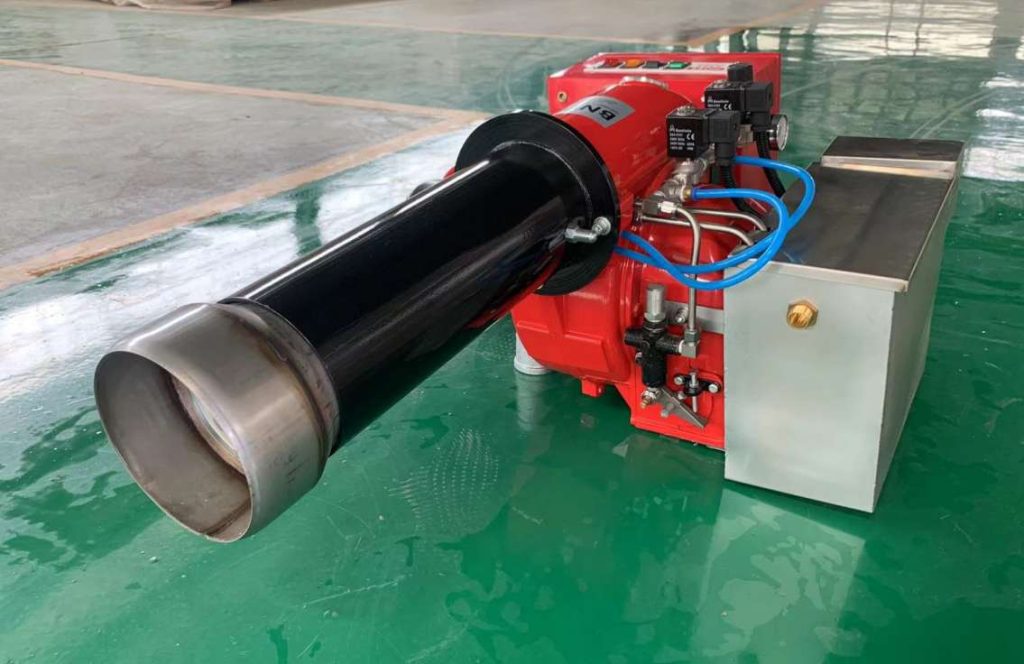
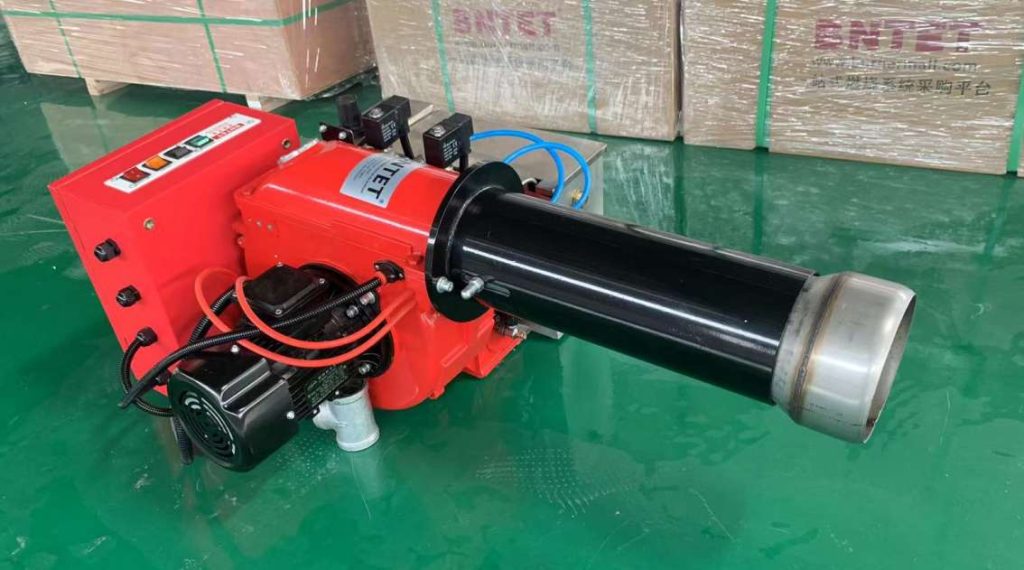
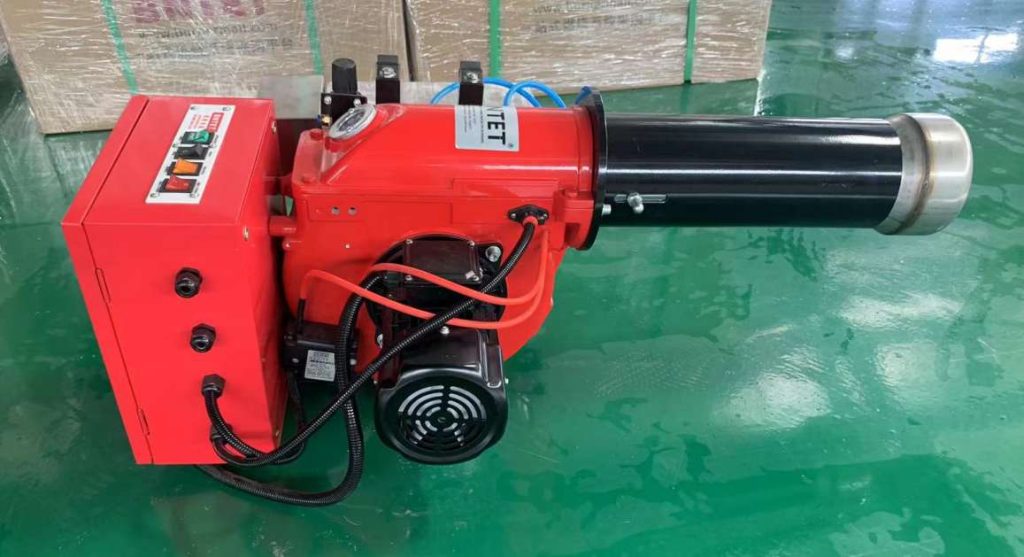
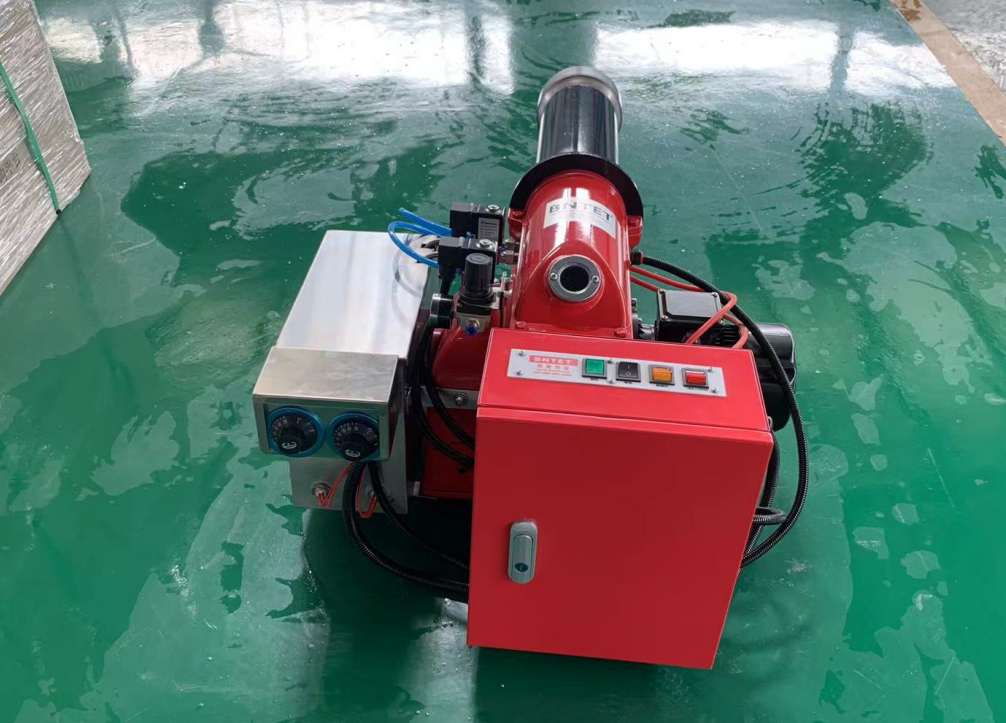
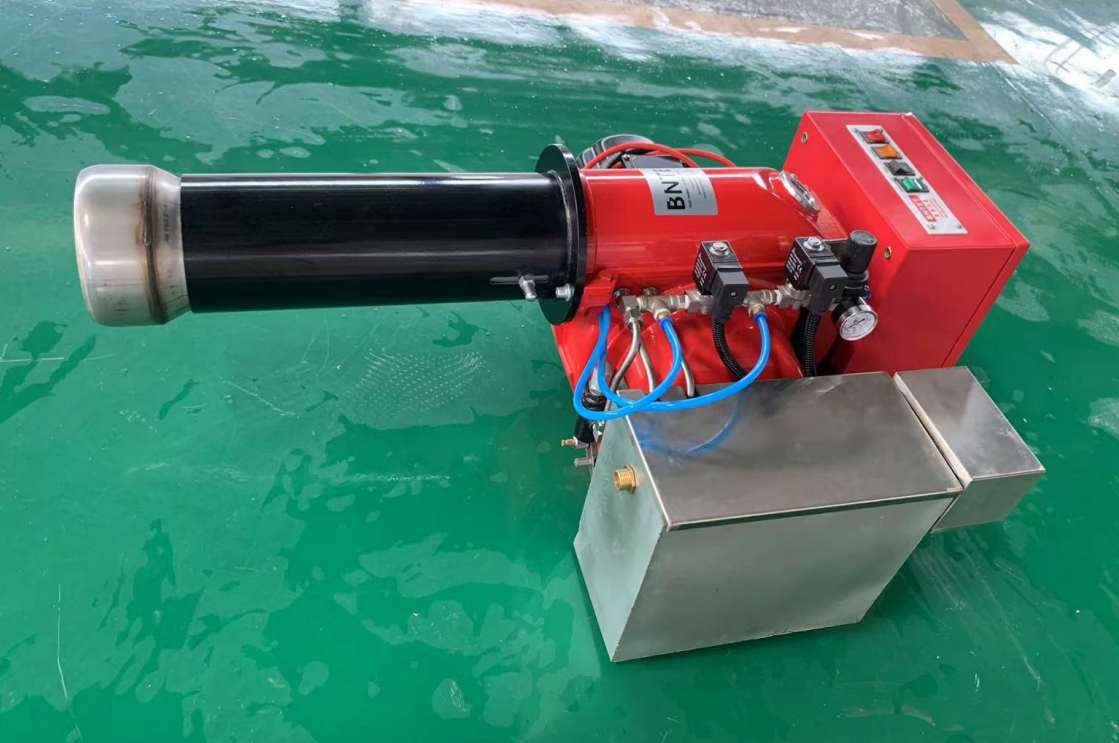
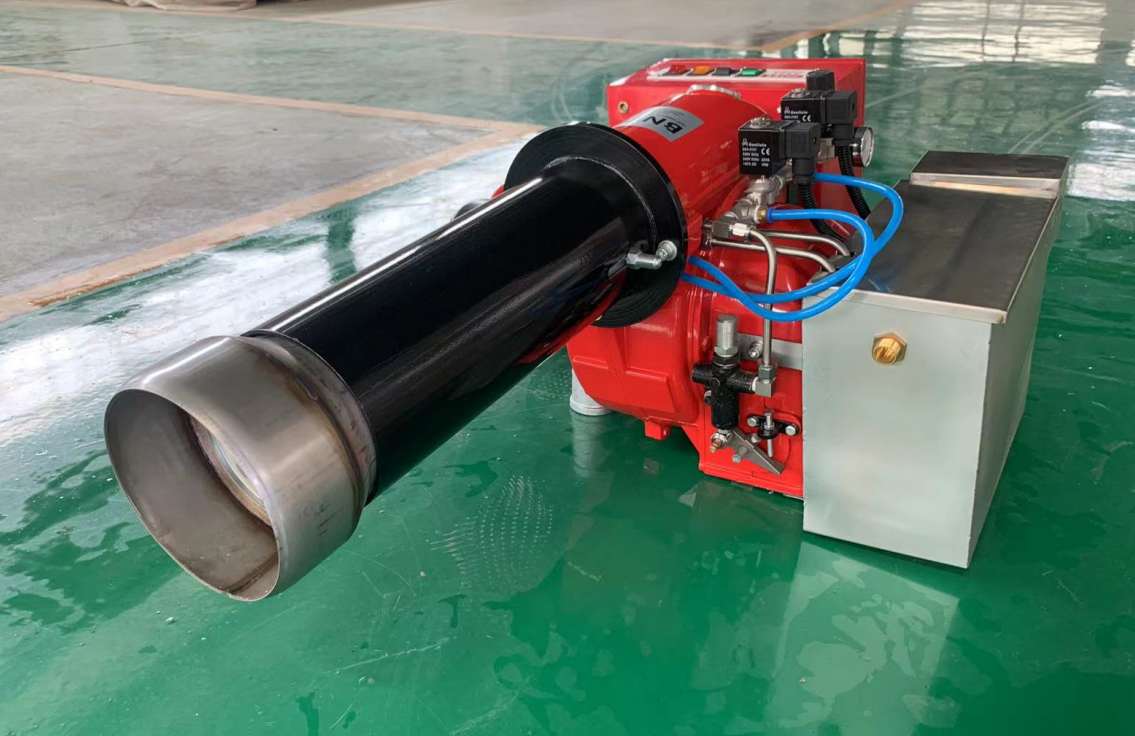
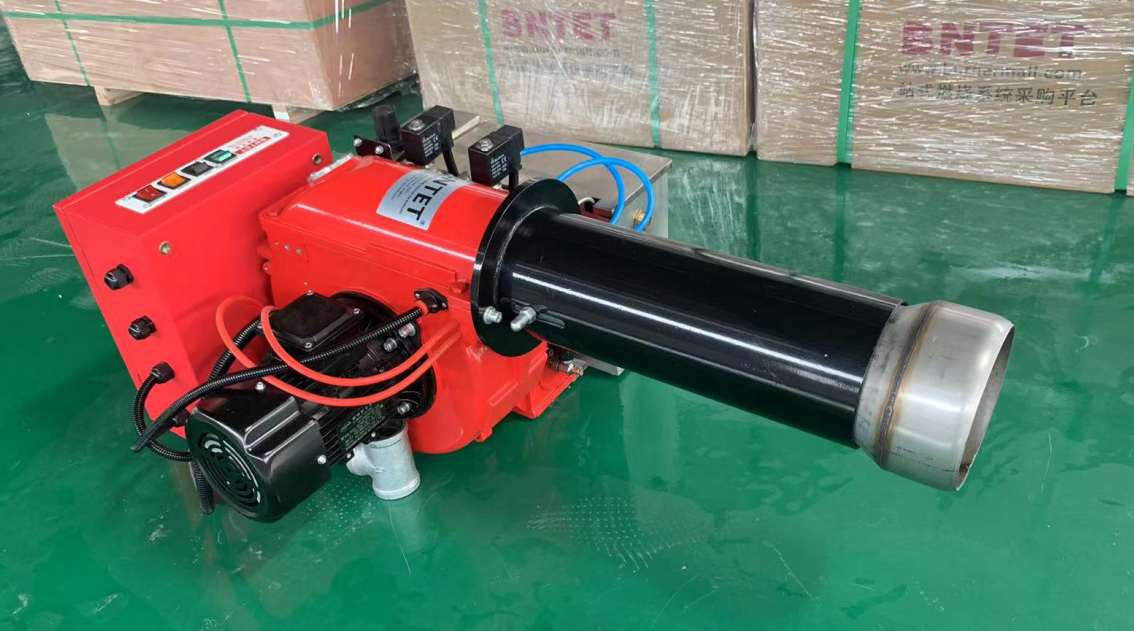
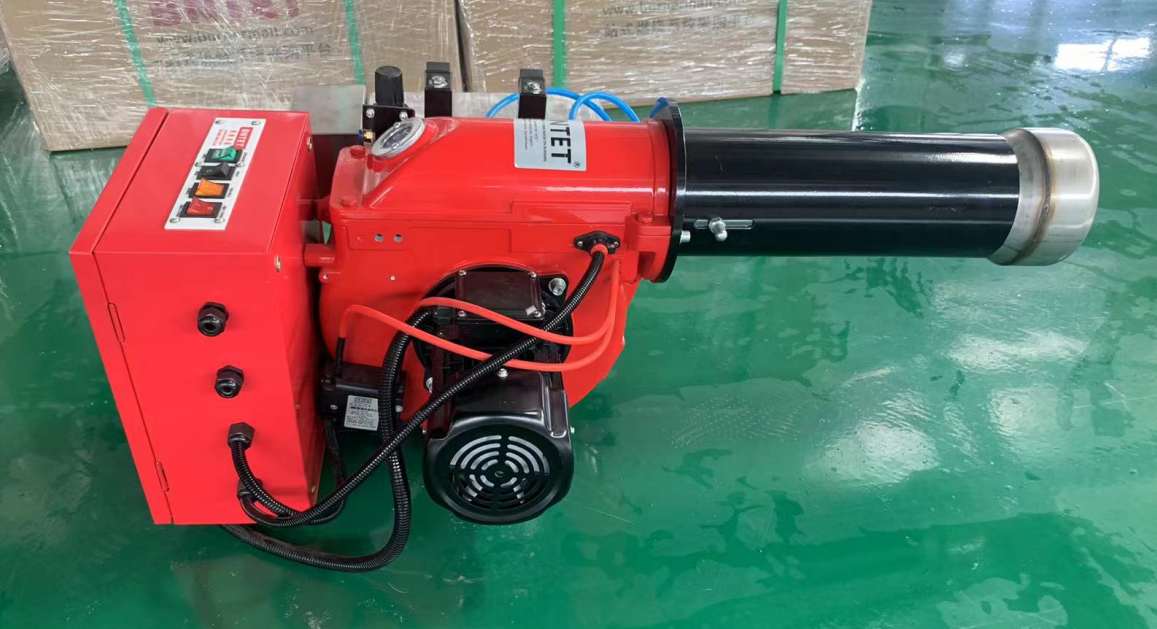
BNW-20 Waste Oil Burner
The BNW-20 model stands out in our waste oil burner range due to its precision-engineered combustion head and enhanced fuel-atomization system, designed specifically for highly efficient waste oil recovery. As a robust, high-performance model from our specialist “BNW” series, the BNW-20 is optimized for the clean and high-capacity utilization of waste oils. This unit benefits from an advanced combustion management system that ensures complete fuel oxidation, effectively minimizing emissions while maintaining a powerful and stable thermal output throughout intensive operations.Features
Unique Design Advantages
The BNW-20’s precision-engineered combustion head and integrated fuel-atomization system provide superior thermal efficiency and air-flow dynamics compared to conventional waste oil burners. Combined with its compact, industrial-grade stainless steel construction, this burner maximizes operational reliability while ensuring complete fuel combustion and minimal emissions, making it ideal for facilities with consistent heating demands.
Versatile Fuel Processing
With advanced technical features, including automated one-stage control, a high-efficiency motor, and optimized internal insulation, the BNW-20 provides exceptional suitability for processing diverse waste oil streams. This versatility makes it a comprehensive solution for industrial facilities seeking sustainable and cost-effective energy recovery while maintaining compliance with operational standards.Why Choose BNW-20?
- Corrosion-Resistant Stainless Steel Construction: The interior is engineered with high-grade stainless steel to prevent corrosion, ensuring maximum durability and long service life even when processing diverse oil types.
- Universal Waste Oil Compatibility: Designed for exceptional versatility, this unit can utilize various flowable waste oils, including corrosive oil, chemical oil, tire oil, and coal tar, providing a sustainable energy solution.
Other Features
- Enhanced Operational Safety – Equipped with automated safety protocols to protect operators during startup and maintenance, ensuring a reliable and hazard-free working environment.
- Optimized Thermal Dynamics – Engineered with advanced airflow dynamics for consistent heat transfer, maximizing energy recovery from every drop of waste oil processed.
- Advanced Integrated Safety Systems – Comprehensive operator and equipment protection with real-time flame monitoring and automated gas-leak detection.
- Smart VFD Advanced Control Panel – Sophisticated monitoring and operation interface with variable frequency drive integration for precise air-fuel ratio modulation.
- Automated Gas Train Valves – Effortless and precise control of high-volume fuel flow using premium automated valve trains for heavy-duty operation.
- Optimized Blast Pipe Design– Superior aerodynamics and gas-flow distribution within the blast pipe for enhanced flame stability.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
Technical Specifications
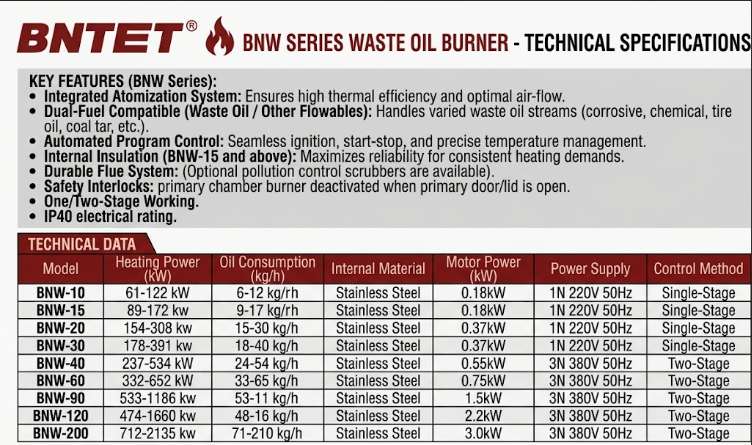
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.