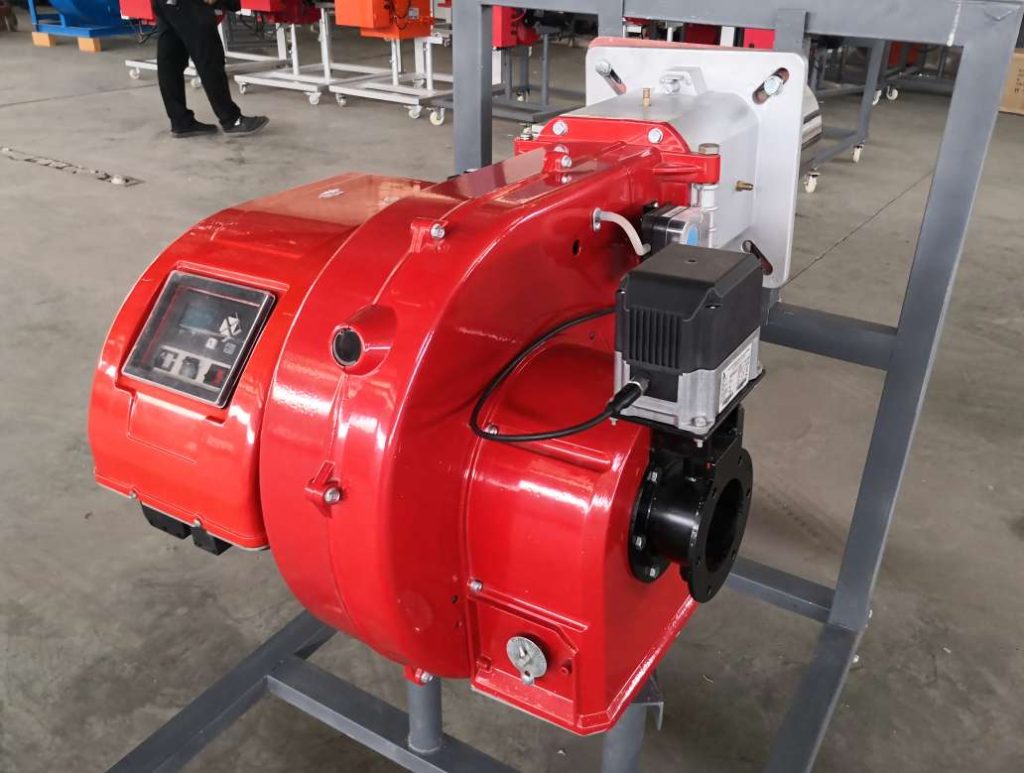
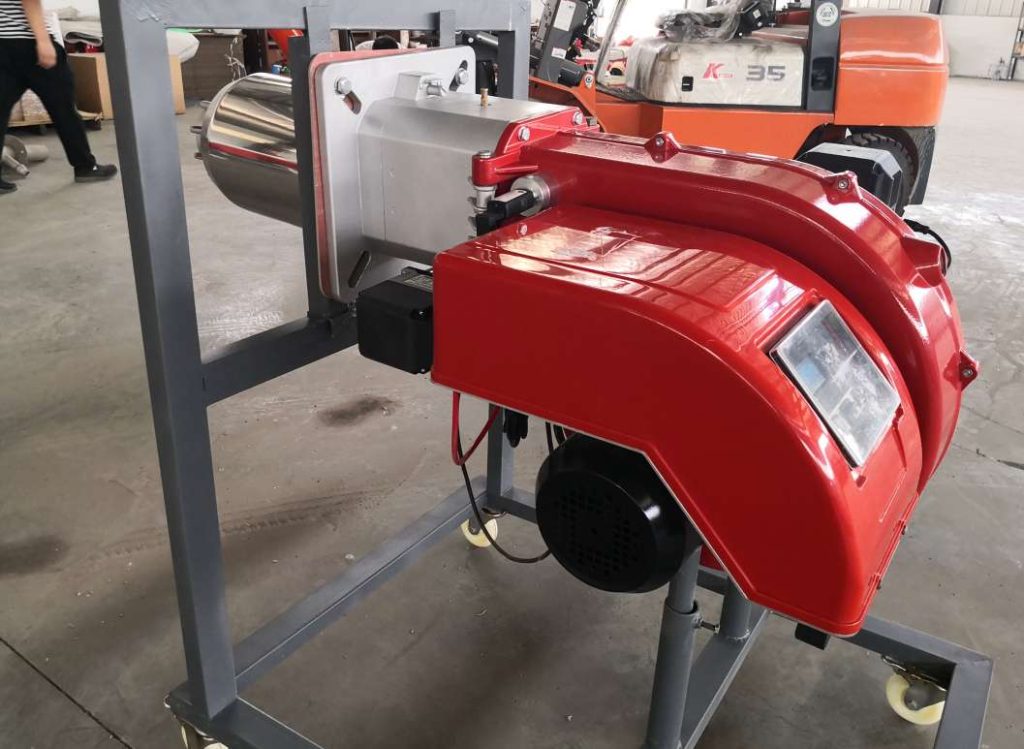
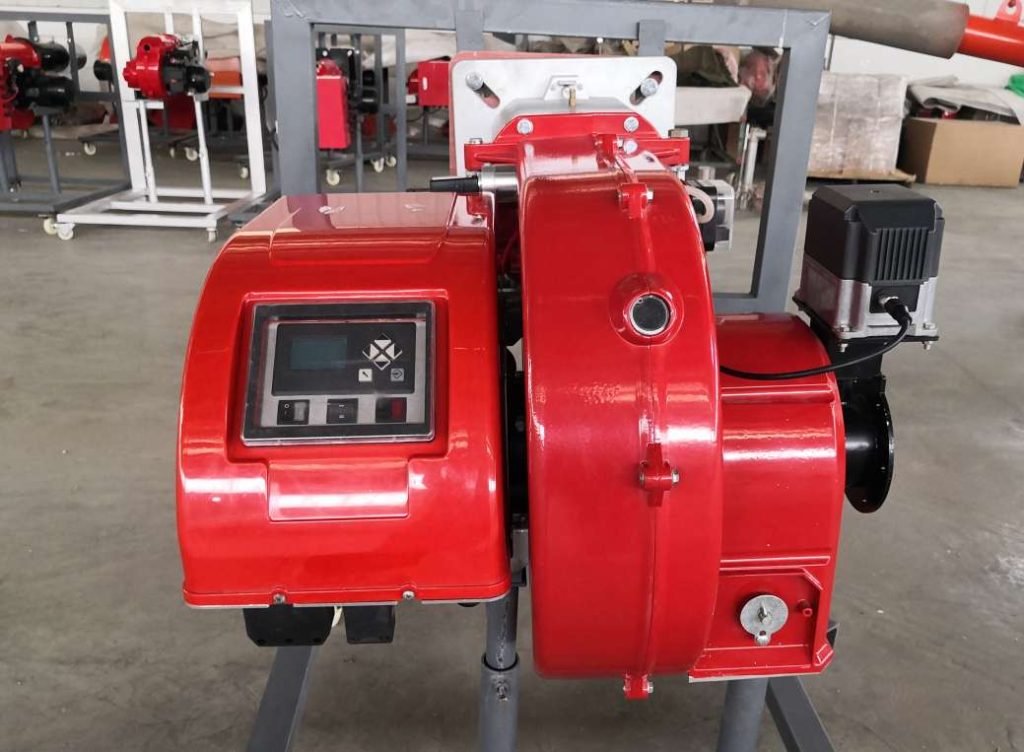
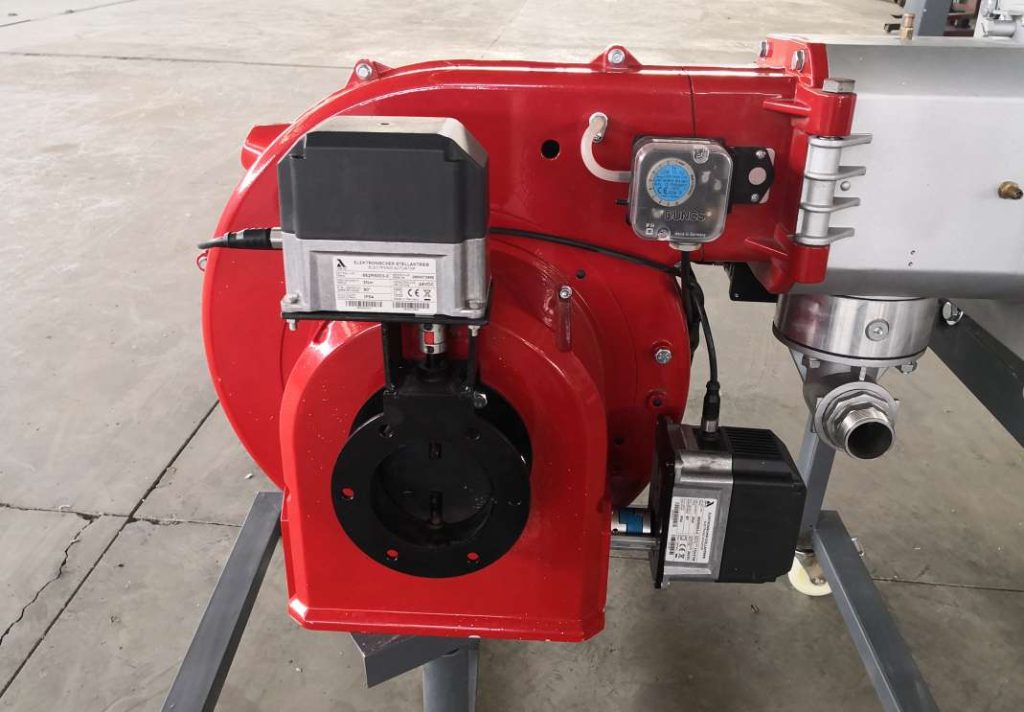
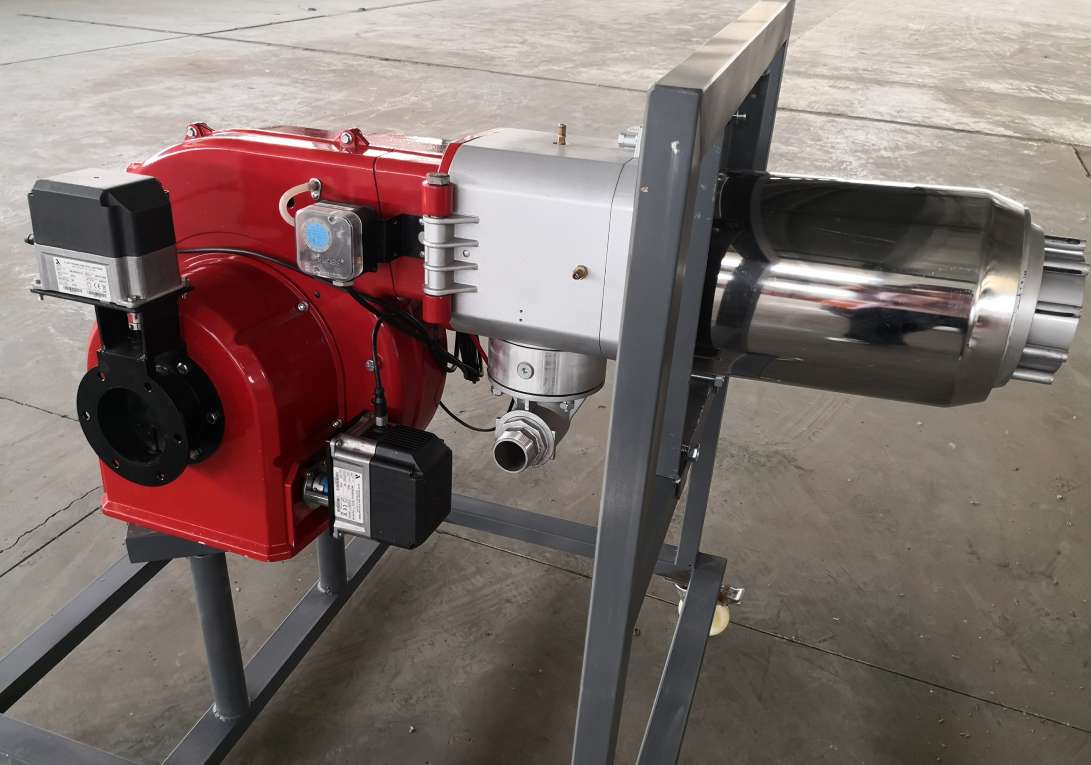
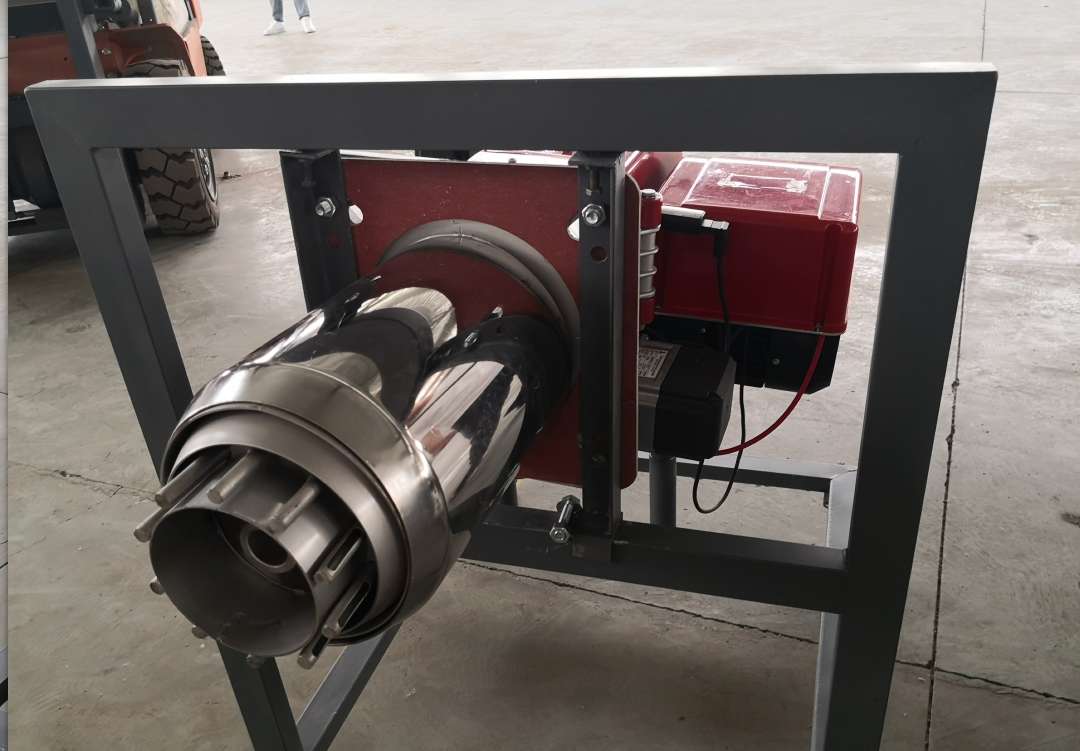
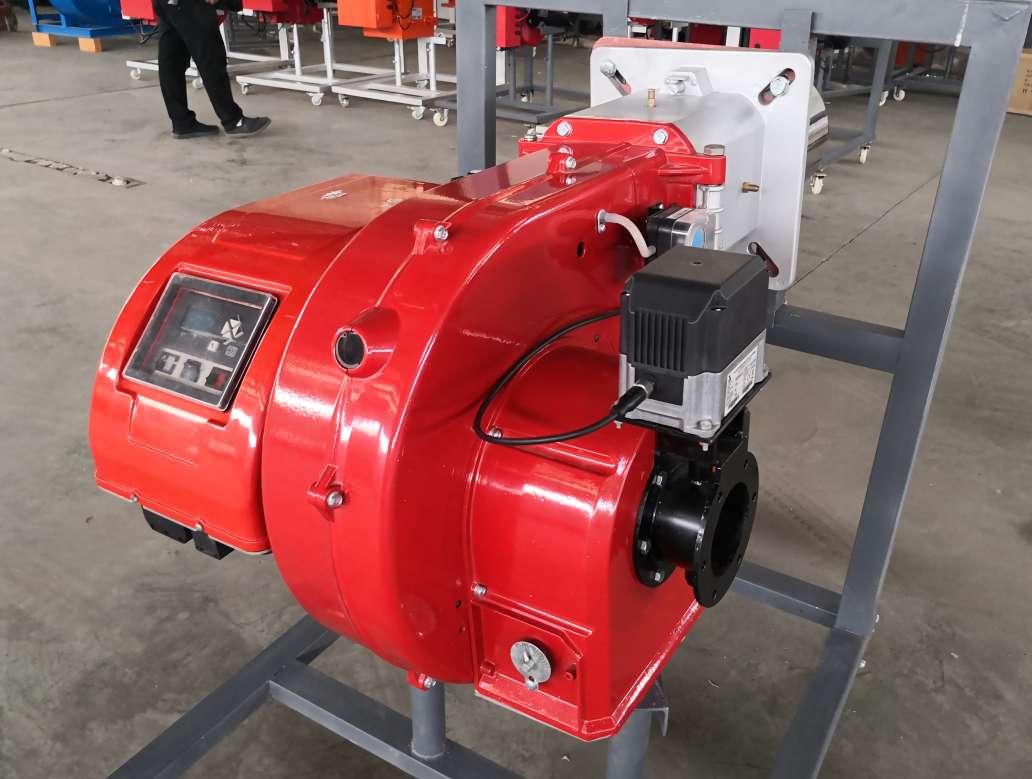
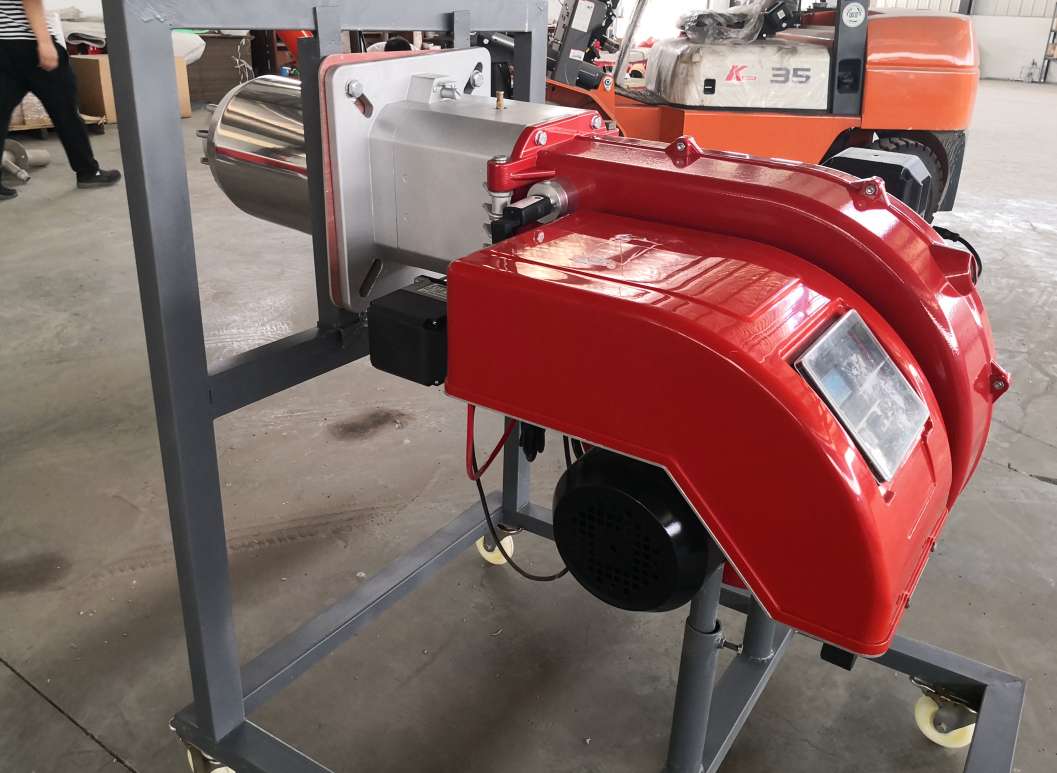
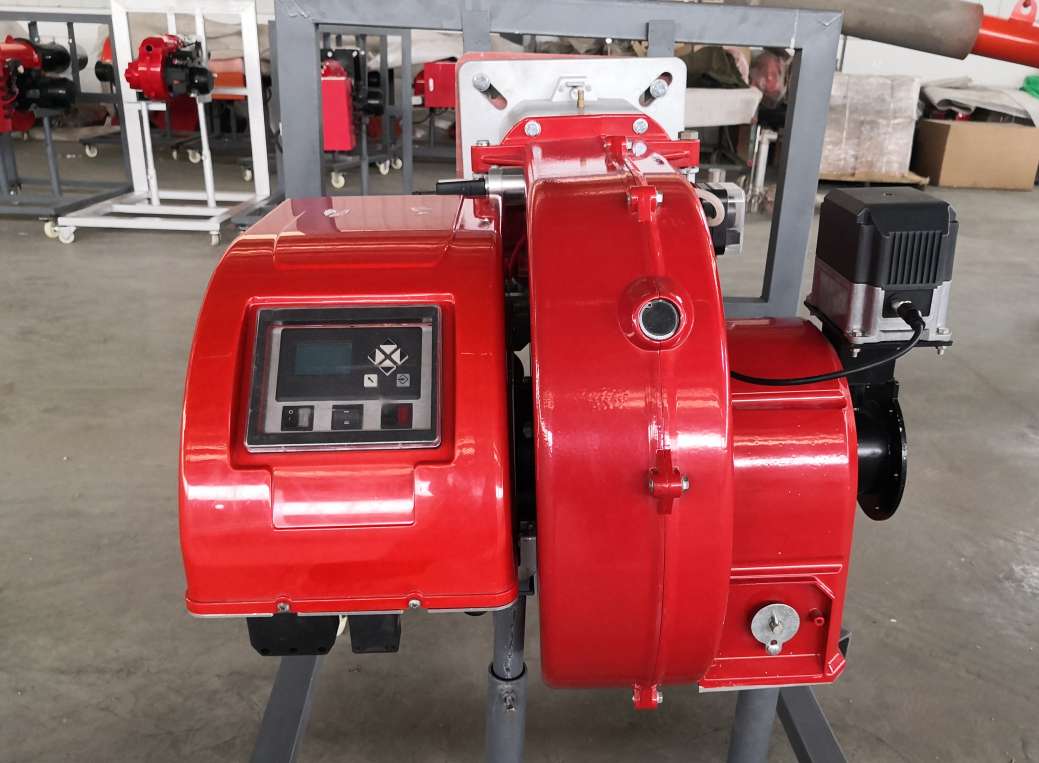
BNLX Low-NOx Burner Series
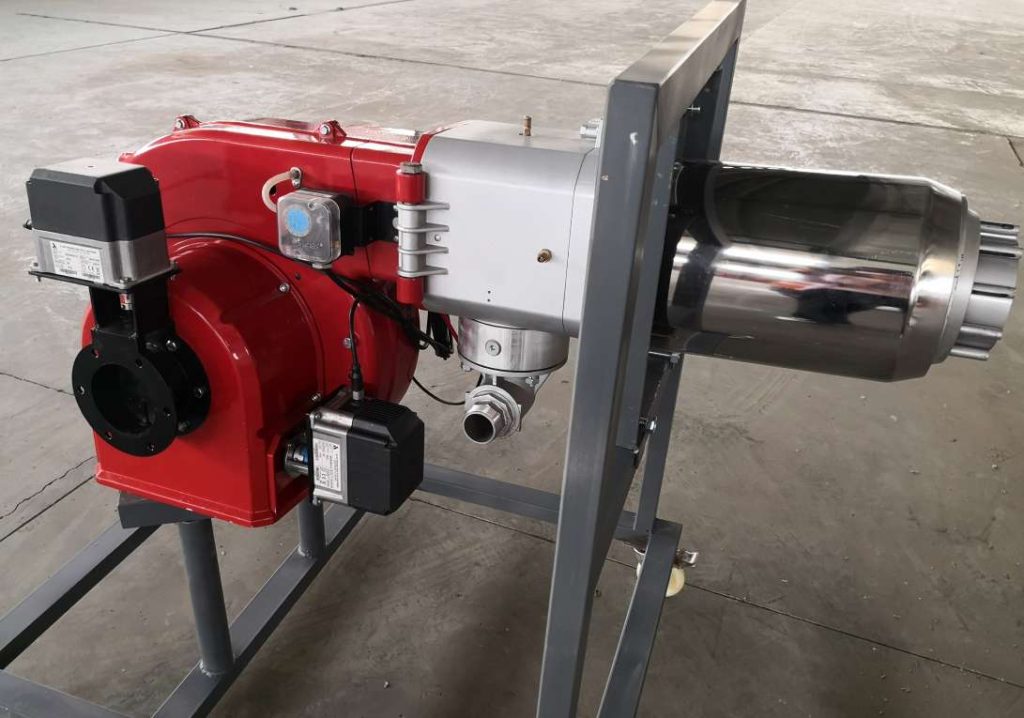
The BNLX series stands as one of the flagship models in our eco-friendly combustion range, engineered specifically to outperform any competitor in its class. This high-capacity, ultra-low NOx burner delivers exceptional thermal efficiency, performance, and scalability to accommodate expanding industrial production lines, capable of delivering immense heat output while strictly controlling emissions. Proven reliable in diverse and demanding industrial environments worldwide, the BNLX series serves as the primary thermal solution for large manufacturing plants, central heating facilities, and industrial boilers. Its impressive capacity and low-emission burn rates make it one of our most sought-after products for substantial energy management and environmental compliance challenges.Features
Unmatched Thermal Capacity & Scalability
The BNLX series offers exceptional heating capacity and precise combustion control, providing the heavy-duty thermal throughput needed for large industrial boilers and centralized district energy operations. Its scalable and modular design allows for seamless integration into expanding production lines as your energy demands increase, protecting your investment as organizational and operational needs evolve.
Superior Performance in Demanding Environments
Developed by a team of highly skilled combustion engineers, our high-capacity low-NOx burners incorporate premium components and intuitive safety design elements. This ensures reliable, uninterrupted 24/7 operation and peak fuel efficiency even under the most demanding industrial loads and strict environmental regulations.Why Choose BNGL-85P?
- Staged Air-Fuel Combustion: Optimized low-NOx combustion achieved through precision staged-air and staged-fuel technology for different firing rates.
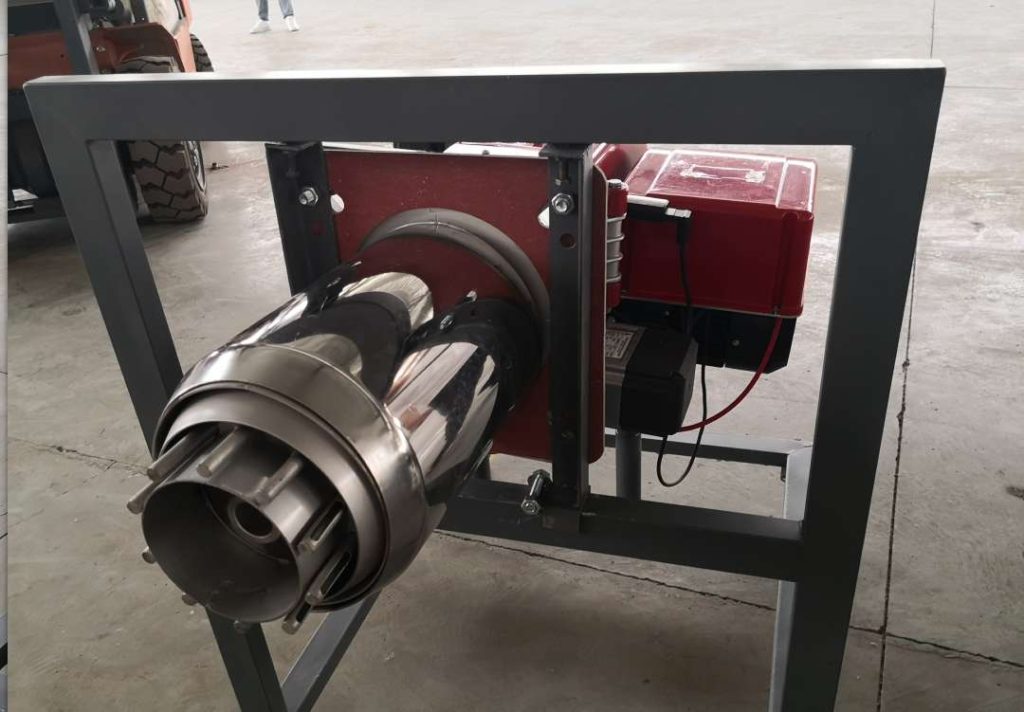
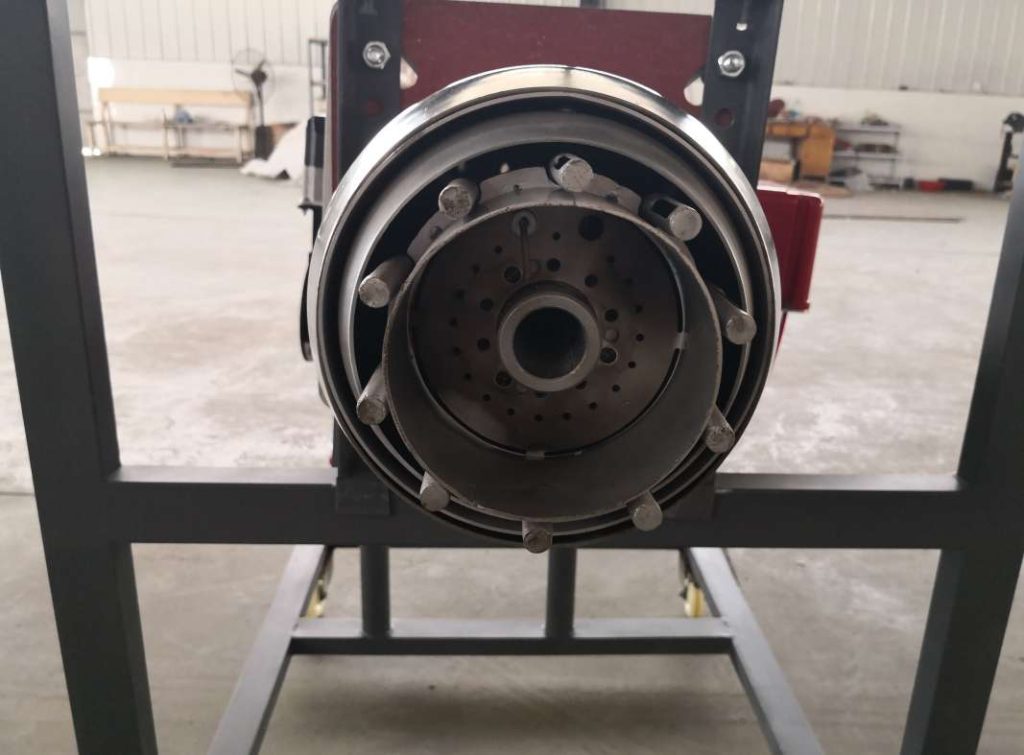
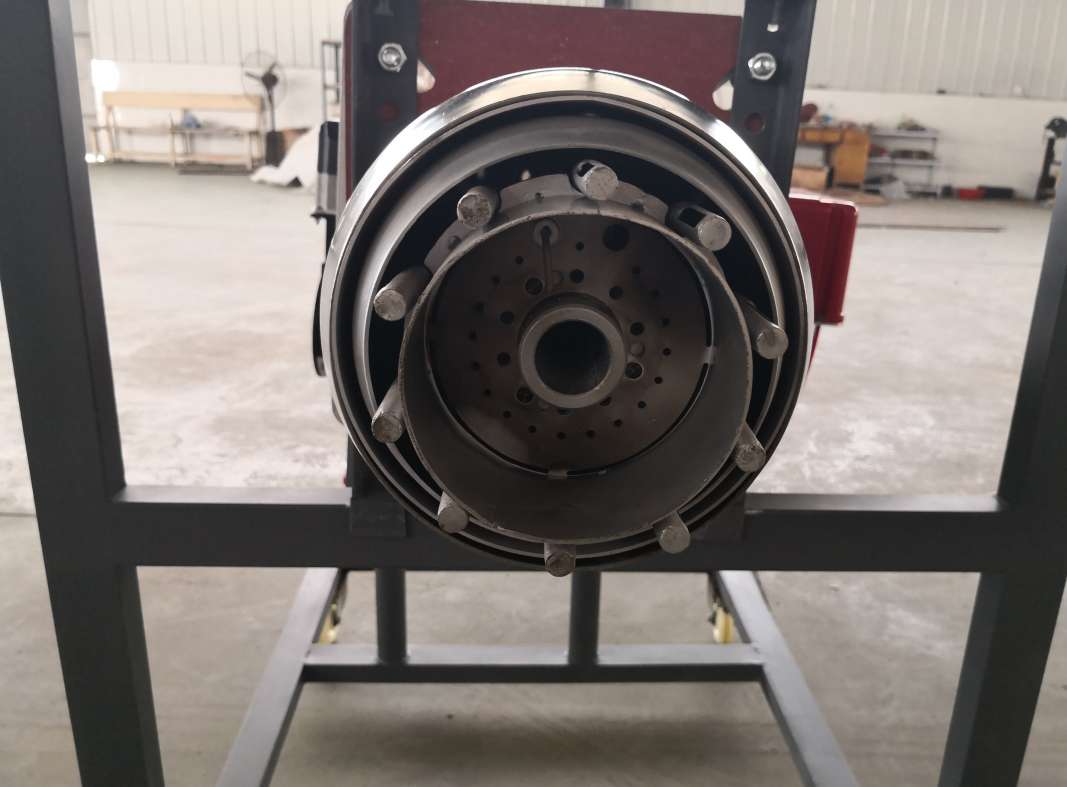
- High-Capacity Combustion Head: Accommodates large-scale industrial thermal demands with high-volume, robust, and stable flame geometry.
Other Features
- Enhanced Thermal Insulation – Superior casing insulation design minimizes heat loss, ensuring maximum thermal efficiency and reduced fuel consumption.
- Multi-Zone Flame Temperature Control – Precise multi-zone combustion management prevents localized peak temperatures, effectively suppressing NOx formation.
- Advanced Integrated Safety Systems – Comprehensive operator and equipment protection with real-time flame monitoring and automated gas-leak detection.
- Smart VFD Advanced Control Panel – Sophisticated monitoring and operation interface with variable frequency drive integration for precise air-fuel ratio modulation.
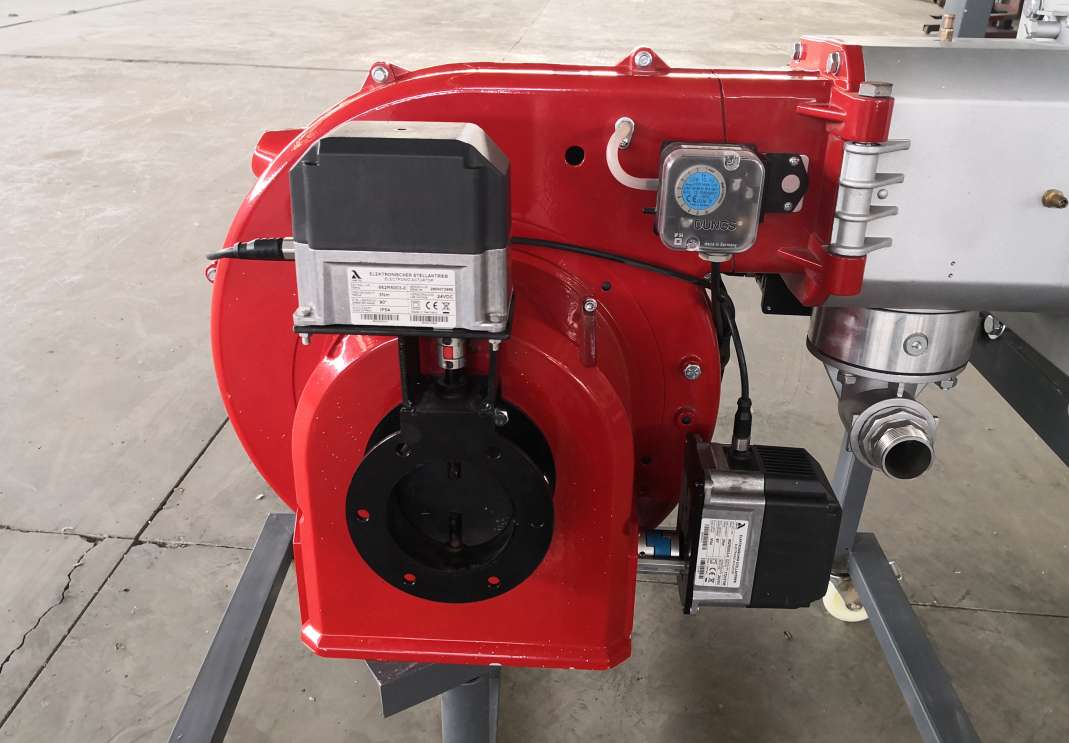
- Automated Gas Train Valves – Effortless and precise control of high-volume fuel flow using premium automated valve trains for heavy-duty operation.
- Optimized Blast Pipe Design– Superior aerodynamics and gas-flow distribution within the blast pipe for enhanced flame stability.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
Technical Specifications
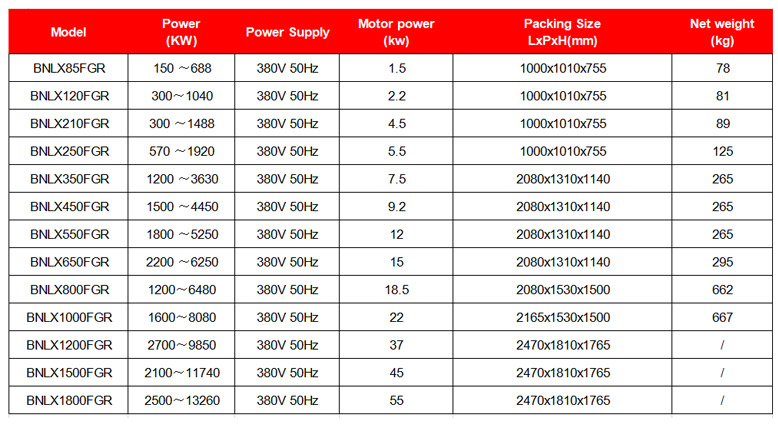
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.