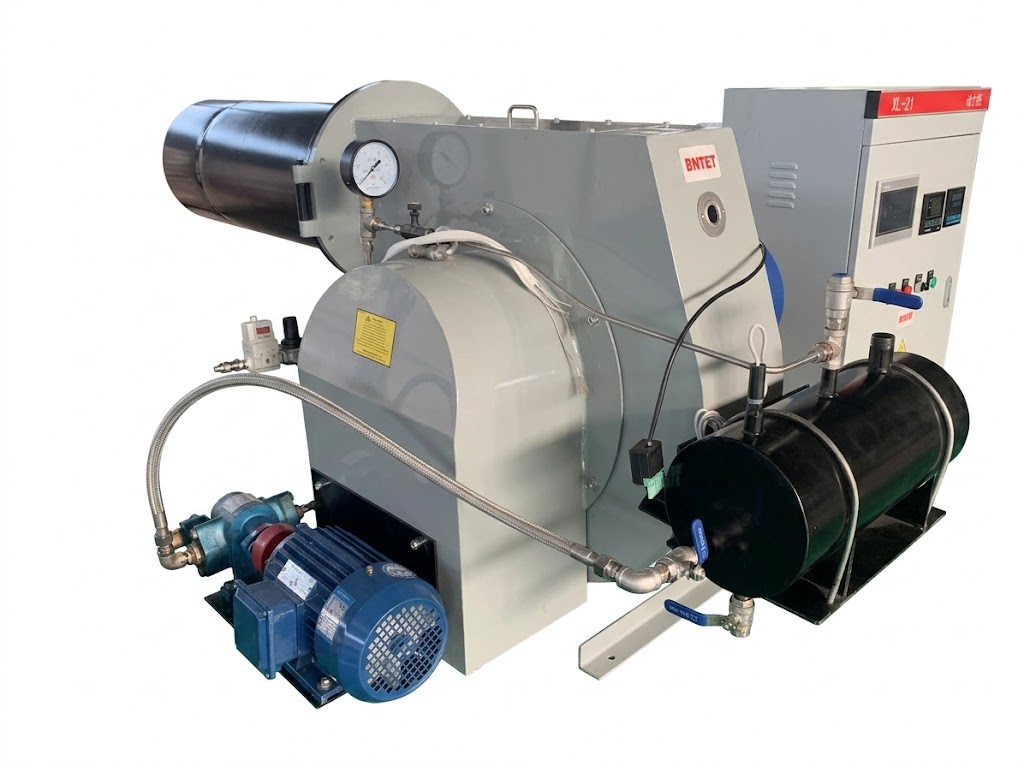
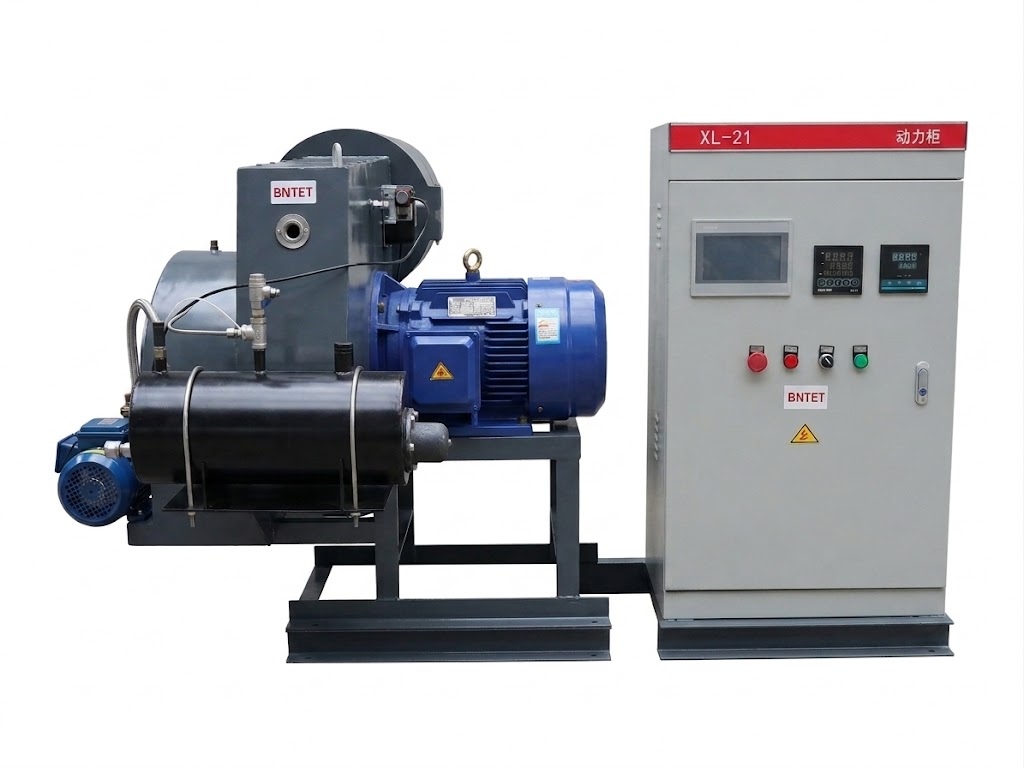
BNH-60G Heavy Oil Burner
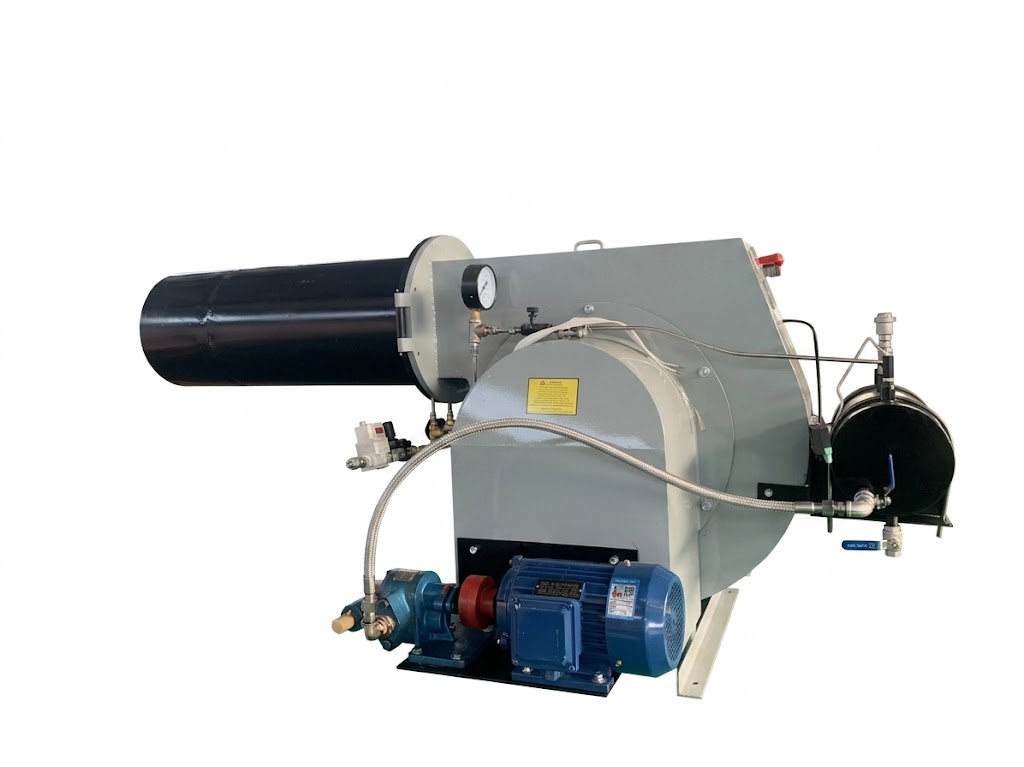
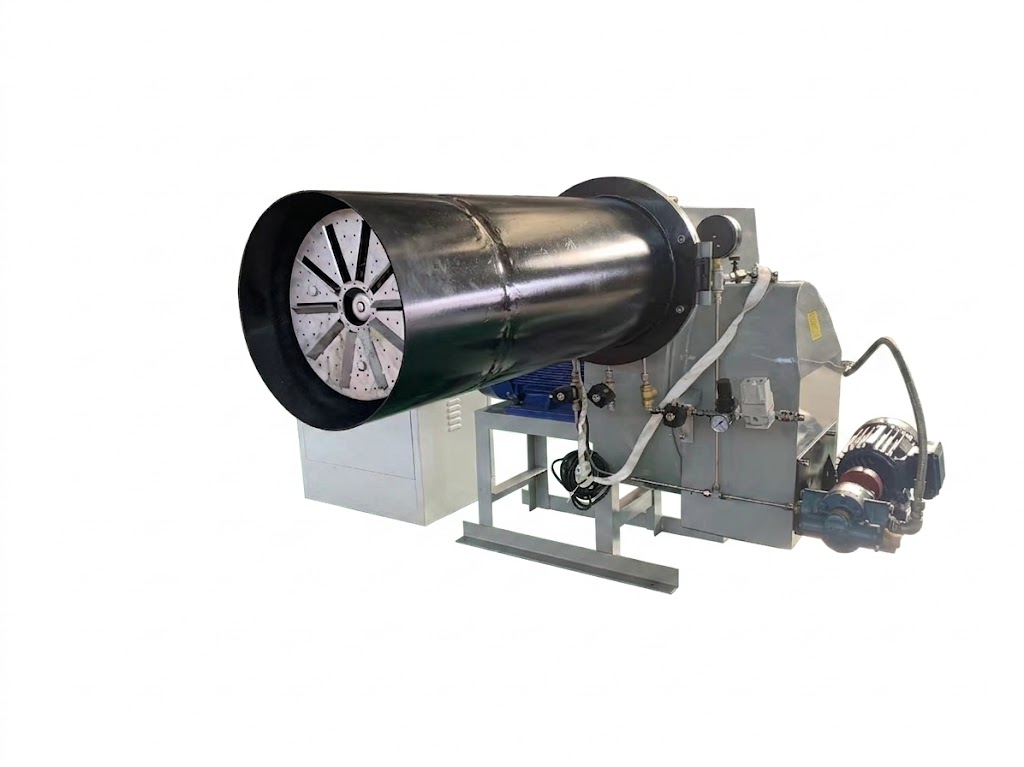
The BNH-60G differs from other burner models in the heavy oil range with its integration of a highly efficient built-in preheating system and a precision-engineered combustion head. The BNH-60G is a medium-capacity model from our range of specialist “BNH” industrial burners that are optimised for heavy fuel oil combustion. This unit benefits from an advanced mechanical atomisation system and precise airflow regulation for the complete burning of high-viscosity fuels, ensuring stable heat output and significantly reduced emissions.Features
Unique Design Advantages
The BNH-60G’s precision-engineered combustion head and integrated preheating system provide superior thermal efficiency and fuel flow dynamics compared to conventional heavy oil designs. Combined with an adjustable blast-pipe and stainless steel nozzle, this burner maximises operational reliability while ensuring complete fuel combustion and minimal emissions, making it the ideal choice for industrial boilers requiring consistent, high-viscosity fuel handling.
Versatile Industrial Performance
With advanced technical features including the precision electronic servomotor for airflow regulation, integrated fuel pre-heater, and premium heavy-duty insulation, the BNH-60G provides exceptional suitability for diverse thermal applications across heavy-duty boilers, industrial dryers, and large-scale heating systems. This versatility makes it a comprehensive solution for industrial facilities seeking stable combustion control and strict compliance with environmental emission regulations.Why Choose BNH-60G?
- Smart Servomotor Airflow Linkage: The system utilizes an electric servomotor for precise airflow ratio management between stage 1 and 2. A key advantage is the automatic air damper closure during shutdown, completely eliminating heat dispersion into the flue, maximizing the boiler’s heat retention and reducing standby energy loss.
- Modular Preheating & Temp Control System: Tailored for high-viscosity heavy oil, the unit features an independent preheater with an integrated thermometer and adjustable controller. Operators can monitor and lock in the optimal atomisation temperature in real-time, overcoming flow and atomisation issues in cold environments to ensure instant ignition and stable operation.
Other Features
- Heavy Oil Optimization – Specially engineered for high-viscosity heavy oil combustion, ensuring stability even under challenging fuel conditions.
- Two-Stage Precision Control – Offers flexible heat load regulation through high/low flame switching, balancing operational efficiency and energy savings.
- High-Efficiency Mechanical Atomisation – Utilizes high-pressure nozzle atomisation to ensure fine fuel dispersion for complete combustion and minimized carbon buildup.
- Intelligent Airflow Management – Features an electronic servomotor for precise airflow regulation in both stages, with an automatic shut-off function to prevent heat loss.
- Visualized Preheating System – Built-in preheating system with an integrated thermometer and adjustable controller to ensure fuel is injected at optimal viscosity.
- Durable Stainless Steel Components – Equipped with stainless steel nozzles and steel deflector disks, significantly enhancing longevity in high-temperature environments.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
Technical Specifications
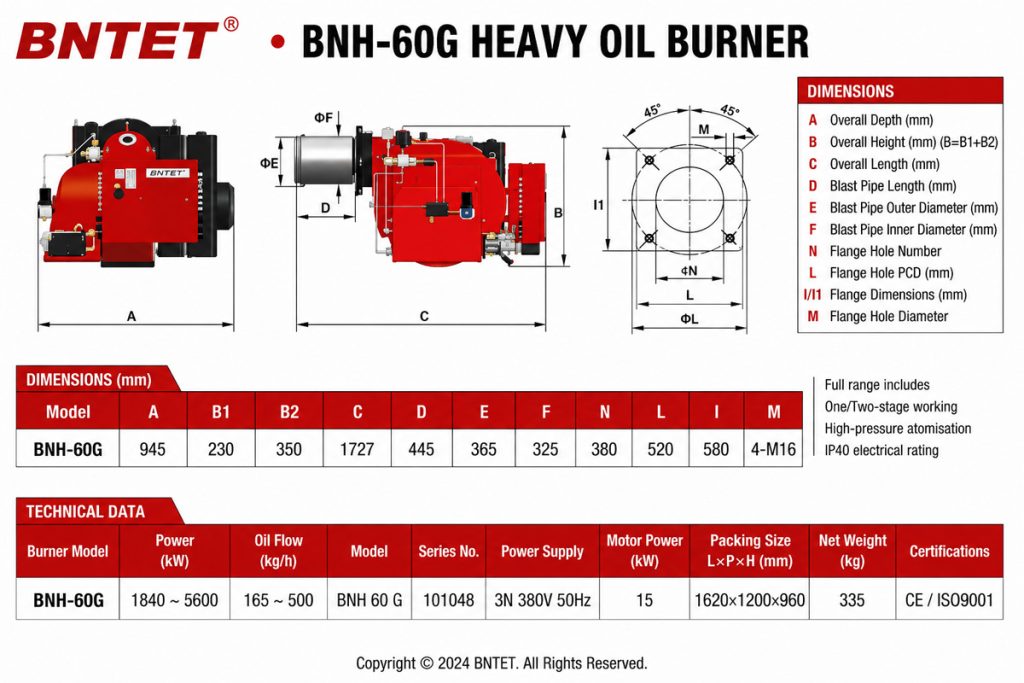
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.