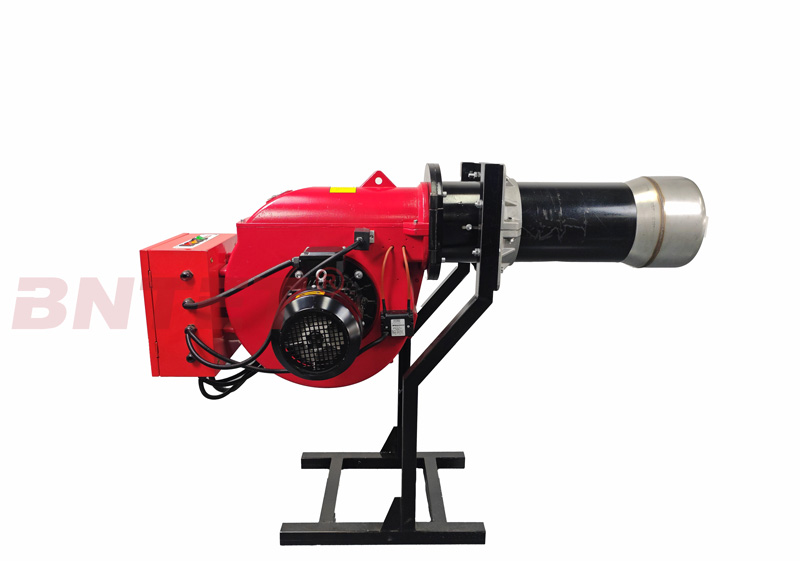
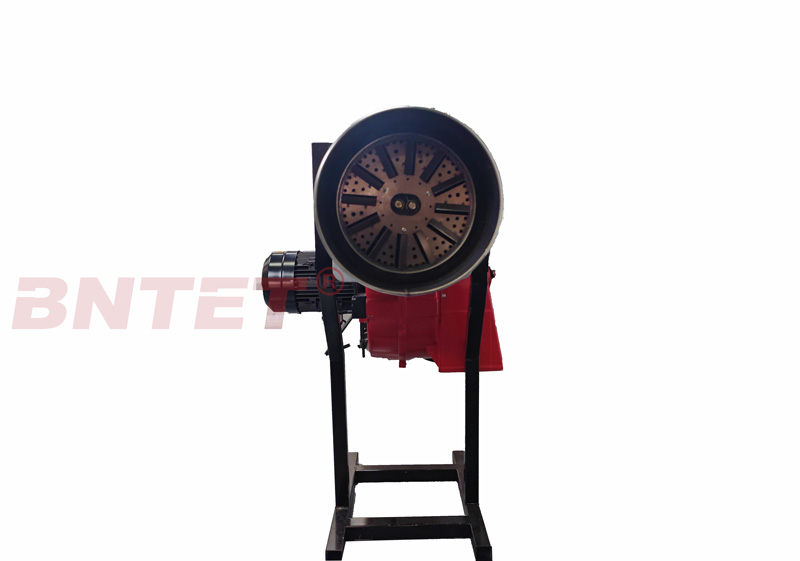
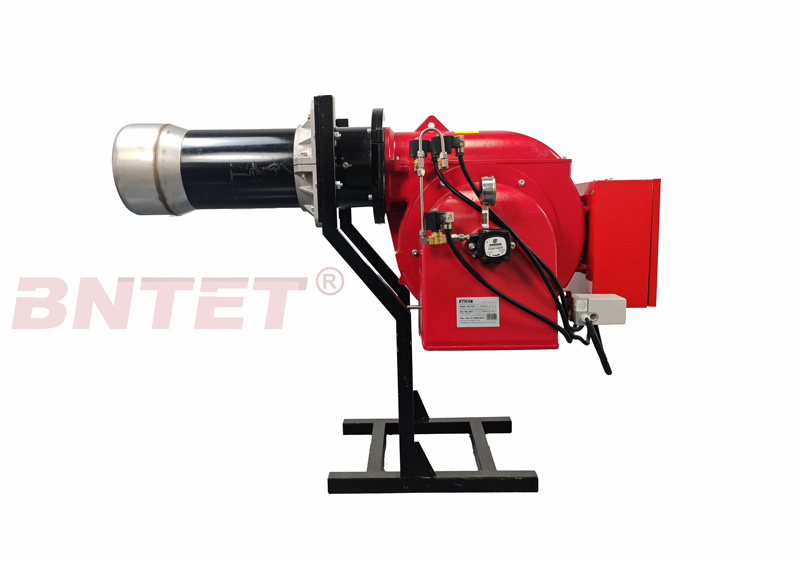
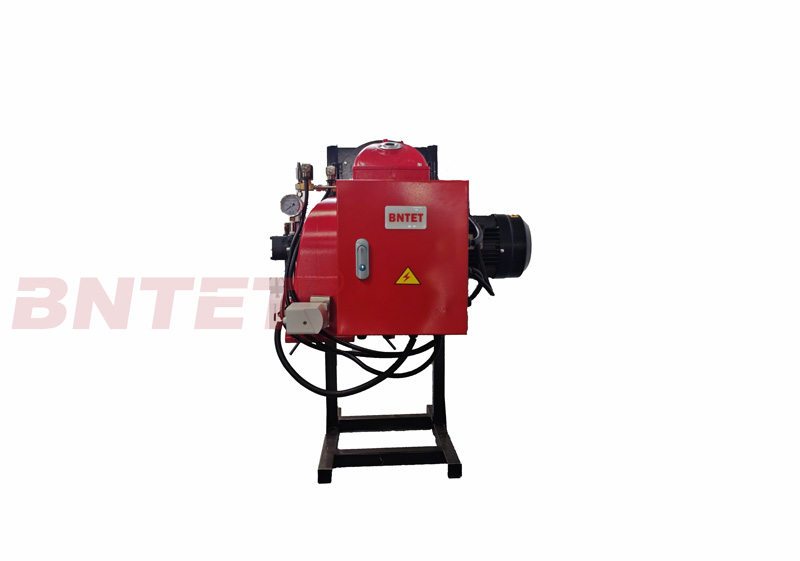
BNL-180P Large Light Oil Burner
The BNL-180P is one of our flagship industrial models—a high-capacity light oil burner specifically engineered for demanding thermal applications, capable of delivering a robust heat output for large-scale operations. Now available with a 2-week lead time. This professional-grade unit features an advanced PLC-integrated control system, high-efficiency combustion air fan, and premium heat-resistant construction to ensure peak performance across industrial boilers, drying equipment, and heavy-duty thermal processing systems. The BNL-180P utilizes precise mechanical atomisation to ensure optimal fuel-air mixing, making it ideal for continuous, high-load requirements. It benefits from an intelligent combustion management system that ensures clean, efficient burning, effectively minimizing emissions and maintaining stable operation throughout its service lifeFeatures
Designed for Heavy-Duty Industrial Heating
A comprehensive thermal solution specifically engineered for large-scale boilers and industrial facilities, featuring advanced mechanical atomisation and a precision combustion head to ensure complete fuel burnout and efficient heat output.
Enhanced Operational Features
Enhanced performance through a dedicated PLC combustion control panel, high-efficiency combustion air fan, and premium heavy-duty insulation, ensuring optimal fuel-air mixing across various load demands while maintaining strict environmental regulatory compliance.Why Choose BNL-180P?
- Non-Dismantle Easy Maintenance Design: The core atomisation unit is engineered as an independent, modular insert. During routine servicing or nozzle replacement, technicians can extract the atomisation assembly without removing the burner from the boiler, significantly slashing downtime and maintenance labor costs.
- Sliding Boiler Coupling Flange System: Features a standard sliding boiler coupling flange designed to adapt perfectly to the head protrusion and wall thickness of various boiler types. This allows easy adjustment of the combustion head’s penetration depth, ensuring perfect alignment with diverse boiler structures for optimal flame positioning.
Other Features
- Dual-Fuel Versatility – Compatible with both light and heavy oil, offering excellent fuel flexibility to meet various operational requirements.
- High-Efficiency Mechanical Atomisation – Utilizes high-pressure nozzle mechanical atomisation to ensure optimal fuel shredding for stable, high-efficiency combustion.
- Complete Boiler Fastening Kit – Equipped with a standard flange and an insulating seal to ensure a secure, heat-resistant connection to the boiler.
- IP40 Industrial Electrical Protection – The electrical system holds an IP40 protection rating, effectively preventing solid particle ingress and ensuring stable operation in harsh environments.
- Efficient Monophase Electric Motor – Driven by a compact monophase electric motor to run both the fan and fuel pump, reducing power consumption and simplifying wiring.
- Optimal Combustion Optimisation – Allows precise regulation of combustion air and the blast-pipe to maintain optimal combustion values and air-fuel ratios.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
Technical Specifications
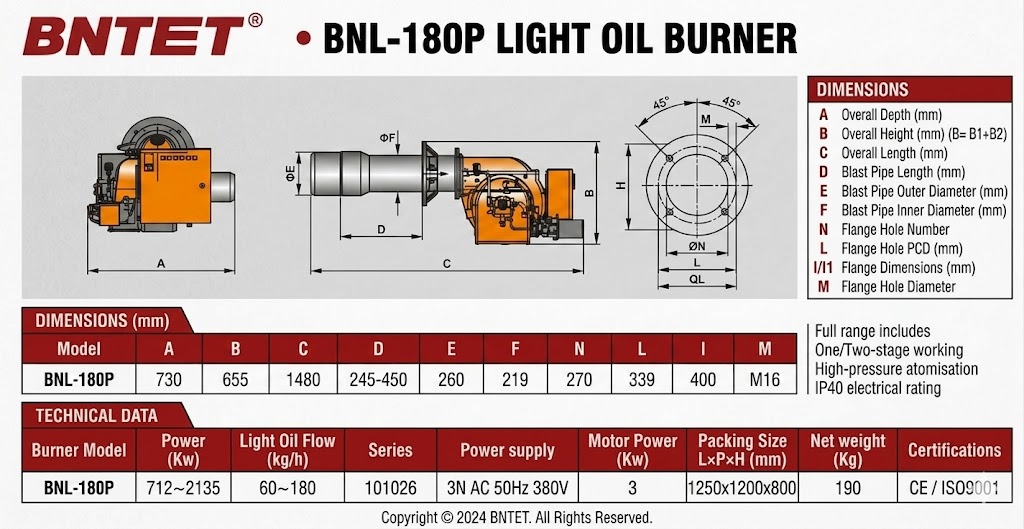
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.