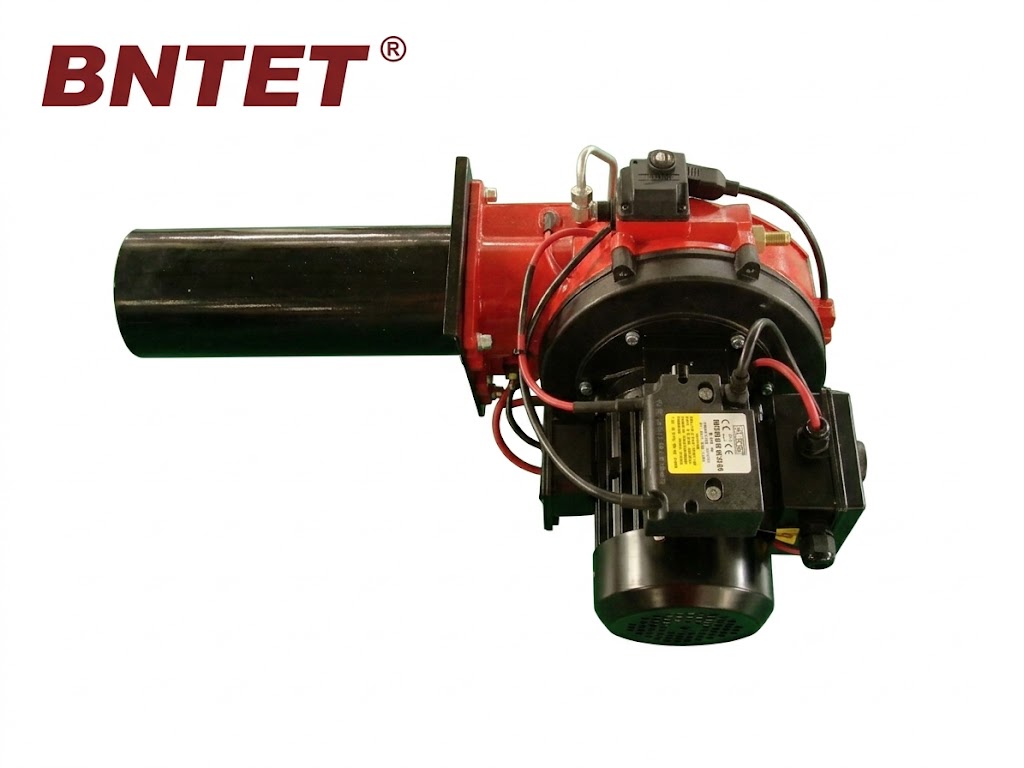
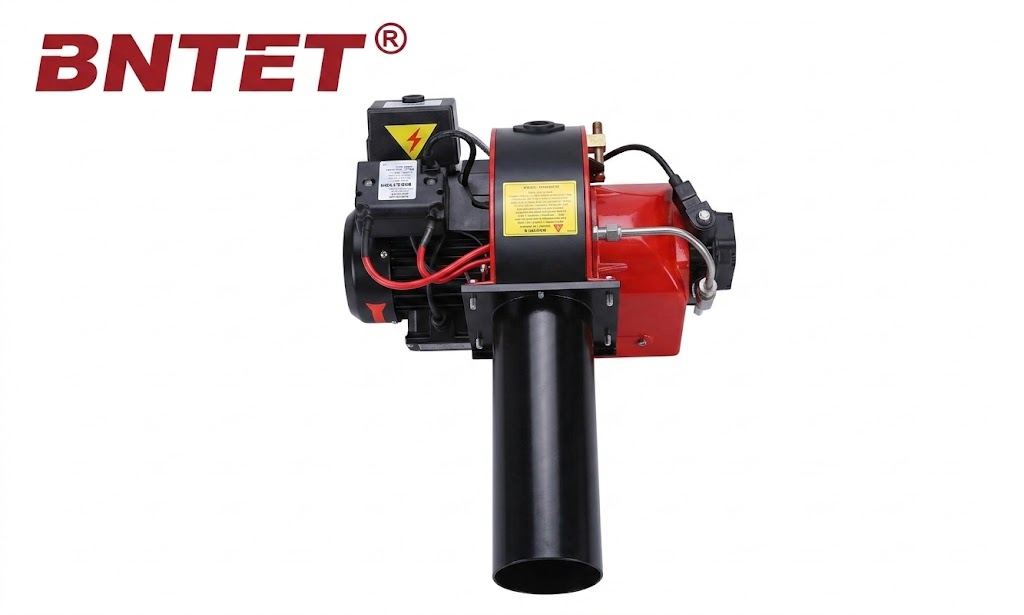
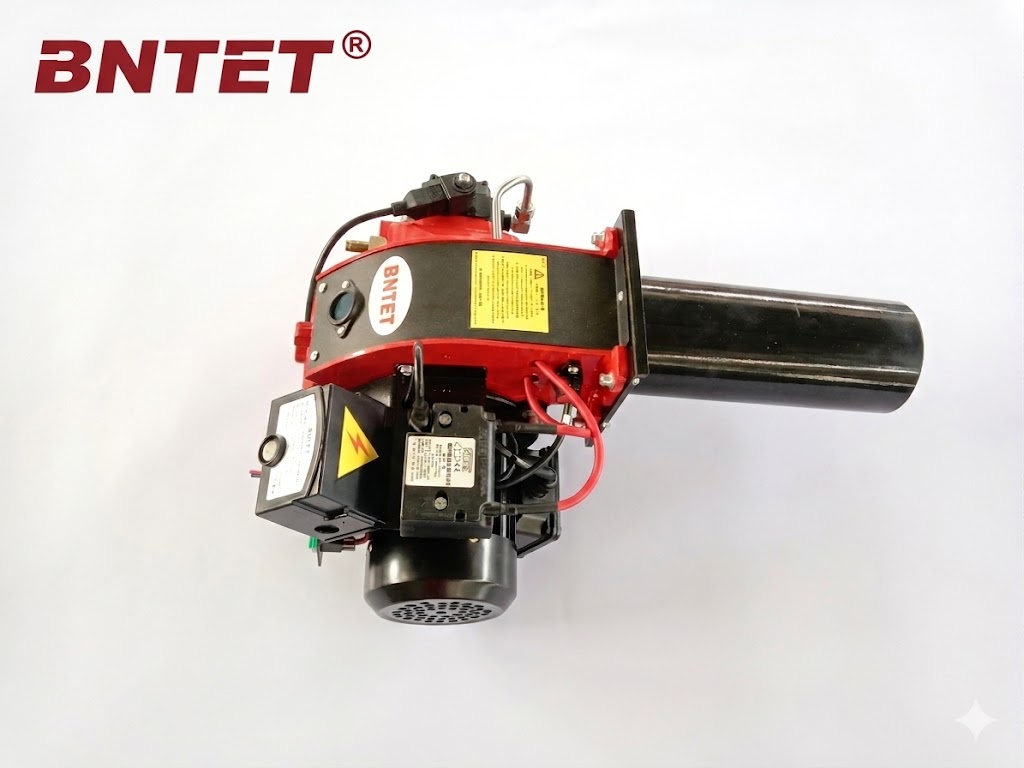
BNL-14 small Light Oil Burner
The BNTET BNL-14 Light Oil Burner is a highly efficient, compact solution specifically engineered for reliable light diesel oil combustion. Designed with a focus on precision and reliability, the BNL-14 utilizes advanced mechanical atomisation technology to ensure complete fuel-air mixing and consistent heat output. This versatile burner is perfectly suited for small to medium-scale heating applications, including commercial boilers, air heaters, drying equipment, and other thermal processing units where space-saving and stable performance are prioritized. Featuring robust ignition, simplified flow adjustment, and a durable IP40-rated industrial structure, the BNL-14 delivers dependable operation, making it the ideal choice for residential heating systems, light industrial manufacturing, and facilities requiring a reliable liquid-fuel heating source in compact spaces.Features
Dual-Fuel Operational Versatility
Designed to handle both light and heavy oil, this burner provides exceptional fuel flexibility, allowing your facility to adapt to varying fuel supply chains without compromising performance.
Versatile Operational Staging
Supports both single and two-stage (on/off) operation, empowering operators to adjust heating output to match specific load demands, thereby optimizing fuel consumption and system longevity.Why Choose BNL-14?
- Advanced High-Pressure Atomisation: Utilizing precision nozzle technology, the system converts liquid fuel into a fine, uniform mist. This ensures complete combustion, significantly increasing heat efficiency while reducing soot accumulation.
- Optimized Combustion Air Management: Equipped with a precision air intake and adjustable blast-pipe system, technicians can easily calibrate airflow to achieve the perfect air-to-fuel ratio for any installation environment.
- User-Friendly Modular Maintenance: Engineered with accessibility in mind, the atomisation unit can be serviced or replaced without the need to detach the burner from the boiler, drastically reducing maintenance downtime.
Other Features
- Precision Hydraulic Flow Regulation – For two-stage models, the integrated hydraulic regulator provides seamless and accurate airflow transitions between the first and second stages, ensuring stable, jitter-free combustion.
- Adaptive Installation Geometry – The innovative sliding boiler coupling flange allows for quick adjustments to head protrusion, ensuring a perfect mechanical fit across a diverse range of boiler types and furnace interfaces.
- Efficient Integrated Power Drive – Features a high-performance monophase electric motor that drives both the fan and the fuel pump, creating a compact, simplified mechanical layout that is easier to maintain and integrate.
- Easy Maintenance Design – The removable combustion unit allows convenient maintenance without removing the burner from the boiler.
- Reliable Optical Flame Security – Utilizes a sensitive photoresistance flame monitoring system to provide continuous, real-time combustion status checks, ensuring immediate safety response and flame stability.
- Stable & Efficient Combustion – Optimised air-gas mixing and adjustable combustion settings ensure stable flame performance and high combustion efficiency.
Applications
This product can be used in a wide variety of locations and settings. Here are some of the most common places where it is used:
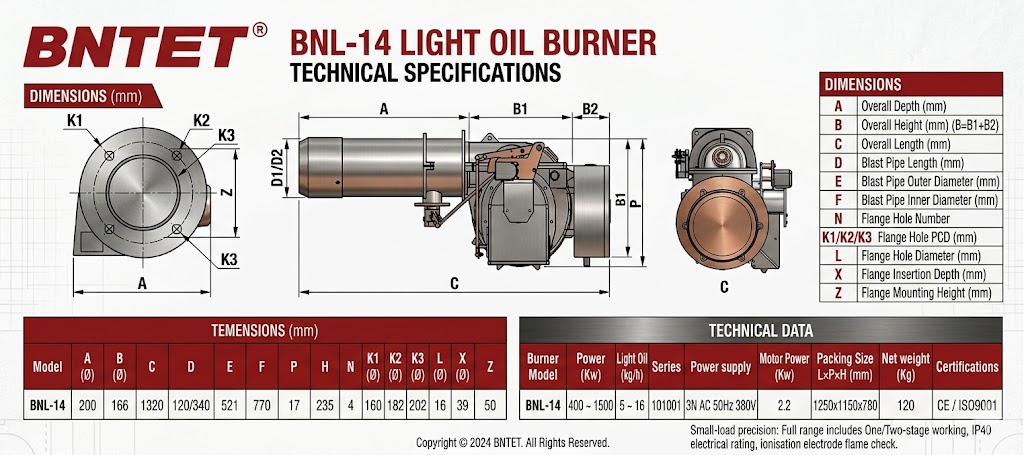
Technical Specifications
Need product advice? Speak to our specialist sales team.
Speak to an expert
Have any questions? Our experts are ready with answers. Contact us today and discover tailored solutions to your specific challenges. Our team brings years of industry experience to every conversation, ensuring you receive practical advice for your project. Don’t navigate these decisions alone — click below to contact us.